Industrial Shelving & Pallet Racking Solutions
Discover a comprehensive selection of industrial shelving and pallet racking systems, designed and manufactured to meet the rigorous demands of modern warehousing and logistics.
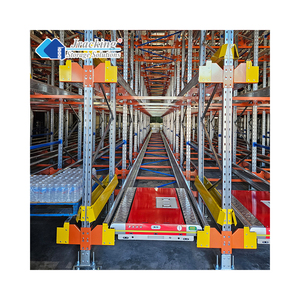
Smart WIFI-Controlled Pallet Racking System
Automated warehouse storage and retrieval system utilizing radio shuttle technology for enhanced efficiency and safety.
Learn More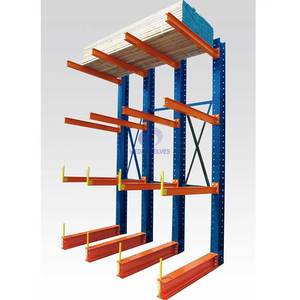
Heavy Duty Aluminium Cantilever Racking
Durable and corrosion-resistant cantilever racks ideal for storing long, bulky items such as pipes, lumber, and metal profiles.
Learn More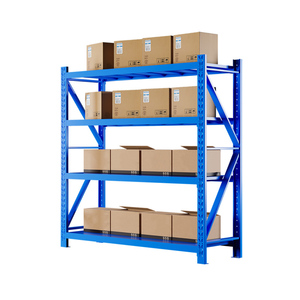
Industrial Warehouse Pallet Racking
Versatile 5-layer racking systems, including tire racks and slotted angle racks, designed for optimal warehouse organization.
Learn More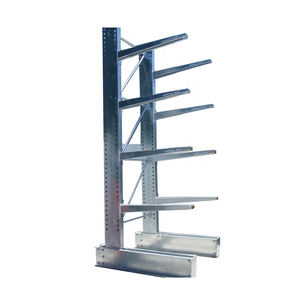
Large Capacity Galvanized Cantilever Racking
Robust and weather-resistant galvanized cantilever racks built for high-volume logistics and outdoor storage applications.
Learn More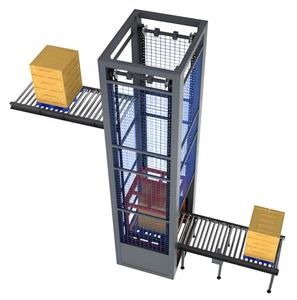
Vertical Pallet Conveyor System
Low-maintenance vertical reciprocating conveyor systems for quick and efficient pallet movement between warehouse levels.
Learn More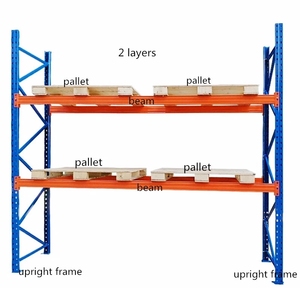
Metal Pallet Racking & Carpet Shelving
Specialized metal pallet racks and hanging carpet shelf racks, designed for efficient storage of textiles and similar items.
Learn More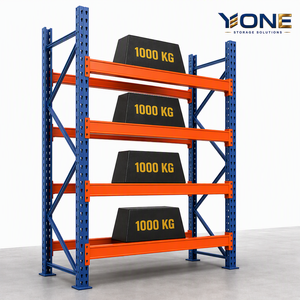
Heavy Duty Steel Pallet Racking
Durable steel storage racks engineered for industrial warehouses, offering superior strength and safety accessories.
Learn More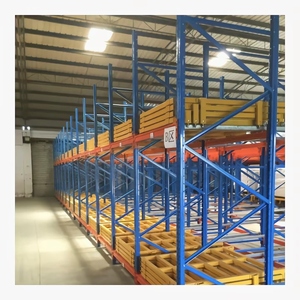
Adjustable Push Back Pallet Racks
High-density storage solution with adjustable push-back racks designed for efficient warehouse pallet organization and retrieval.
Learn MoreDriving Warehouse Efficiency with Advanced Shelving
Our industrial shelving and pallet racks are built with E-E-A-T principles at their core, ensuring you receive solutions that are not only durable and efficient but also backed by extensive experience and expertise.
Robust Construction
Fabricated from high-grade steel and subjected to rigorous quality control, our racks withstand heavy loads and demanding operational cycles.
Customizable Designs
Tailored to your specific inventory, space constraints, and operational needs, offering a perfect fit for any warehouse layout.
Enhanced Safety Features
Incorporating safety guards, anti-collapse systems, and secure connections to ensure a safe working environment for personnel and products.
Optimized Space Utilization
Designed to maximize vertical and horizontal space, increasing storage density and reducing the overall footprint required for inventory.
The Future of Industrial Shelving & Pallet Racking
Stay ahead of the curve with our insights into evolving warehousing technologies and procurement trends in industrial storage solutions.
Automation Integration
The increasing demand for automated guided vehicles (AGVs) and robotic systems is driving the development of shelving that seamlessly integrates with these technologies, optimizing throughput and reducing labor costs.
TRENDING NOWData-Driven Warehousing
IoT sensors integrated into shelving systems will provide real-time data on inventory levels, environmental conditions, and structural integrity, enabling predictive maintenance and smarter operational decisions.
EMERGING TECHSustainable Materials & Practices
Increased emphasis on eco-friendly materials, recycled content, and energy-efficient manufacturing processes, aligning with global sustainability goals and corporate responsibility.
GROWING DEMANDCommon Questions About Industrial Shelving & Pallet Racks
We understand you need clear answers. Here are frequently asked questions to help you make informed decisions about your industrial storage needs.
What are the primary types of industrial pallet racking?
The most common include selective pallet racks (offering direct access to each pallet), drive-in/drive-thru racks (for high-density storage), push-back racks (for LIFO inventory), and flow racks (for FIFO inventory).
How do I determine the right capacity for my pallet racks?
Capacity is determined by the weight and dimensions of your typical loads, the frequency of access required, and your warehouse layout. We recommend consulting with our experts to calculate precise requirements.
What is the typical lifespan of industrial shelving?
With proper maintenance and load adherence, industrial shelving can last 15-20 years or more. Factors like material, coatings, and environmental conditions influence longevity.
Can I get custom-sized shelving or racks?
Absolutely. As an OEM supplier, we specialize in custom solutions. We work with you to design and manufacture shelving and racks that precisely match your specifications.
What safety standards should I consider for pallet racking?
Key standards include load capacity labeling, frame and beam protection, regular inspections, and ensuring racks are properly anchored. Compliance with local building codes is also critical.
How does seismic resistance factor into rack design?
In earthquake-prone regions, racks must be engineered with specific seismic resistance features, including robust anchoring and connection designs, compliant with local building codes like IBC in the US and NBC in Canada.
Our Strengths as Your OEM Supplier
Leveraging extensive industry experience and a commitment to quality, we offer unparalleled advantages in industrial shelving and pallet rack manufacturing.
OEM Expertise
As an Original Equipment Manufacturer (OEM), we possess deep knowledge of product design, materials science, and production processes, ensuring top-tier quality.
Precision Engineering
Our commitment to precision engineering ensures that every component meets exact specifications, leading to superior performance and durability.
Global Supply Chain
Leveraging a robust global supply chain, we ensure timely delivery and competitive pricing for projects of all scales, serving North America and beyond.
Scalable Production
Our manufacturing capabilities are designed for scalability, allowing us to efficiently handle large-volume orders while maintaining exceptional quality standards.
Dedicated Support
From initial design consultation to post-installation support, our dedicated team provides expert guidance and responsive service throughout your project lifecycle.
Innovation Focus
We continuously invest in R&D to bring you the latest innovations in industrial storage, including smart technologies and advanced material applications.
Partner with Us for Your Custom OEM Industrial Shelving Needs
Let's discuss your project requirements. Our team of experts is ready to provide tailored solutions that enhance efficiency, safety, and profitability for your operations.