Empowering Organizations Through Smarter Space
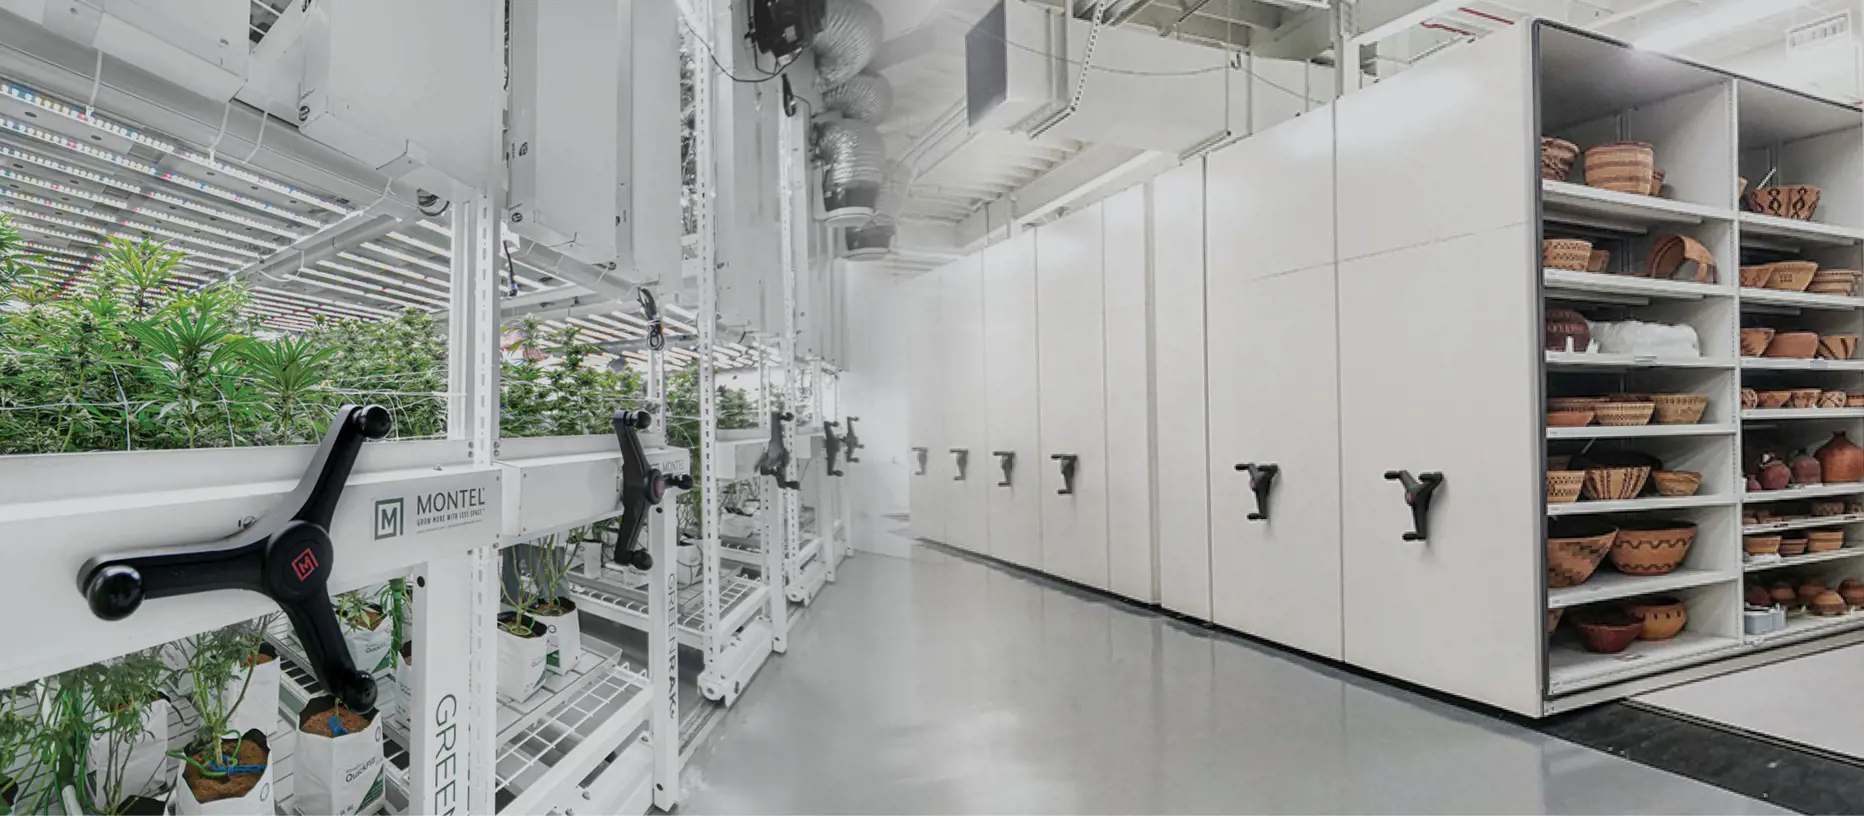
Through continuous engineering innovation and an uncompromising commitment to structural integrity, Montel Shelving Inc. redefines the possibilities of high-density storage and vertical farming.
Our Mission
As a recognized North American leader in innovative high-density mobile shelving and multi-tier grow systems, our mission is to empower global procurement teams, architects, and facility managers by transforming how they store, protect, and grow through intelligent, precision-built space solutions.
Our Vision
Providing global commerce, public institutions, and commercial agriculture with smarter, scalable space to store more, preserve better, and maximize operational profitability within minimal footprints.
A Century of Industrial Excellence
Montel Shelving Inc.'s legacy is grounded in 40 years of heavy electrical and power-grid infrastructure, providing the rigorous foundation for our industry-leading mobile motorized carriages today.
1924Foundation in Heavy Electrical & Mechanical Engineering
Before pioneering compact storage, Montel gained four decades of deep technical mastery participating in the electrical infrastructure, power grid generation, and heavy mechanical works of major hydroelectric power plants in North America. This rigorous background forms the unmatched durability of our drive mechanisms.
1960s – 1970sPioneering Mobile Storage in North America
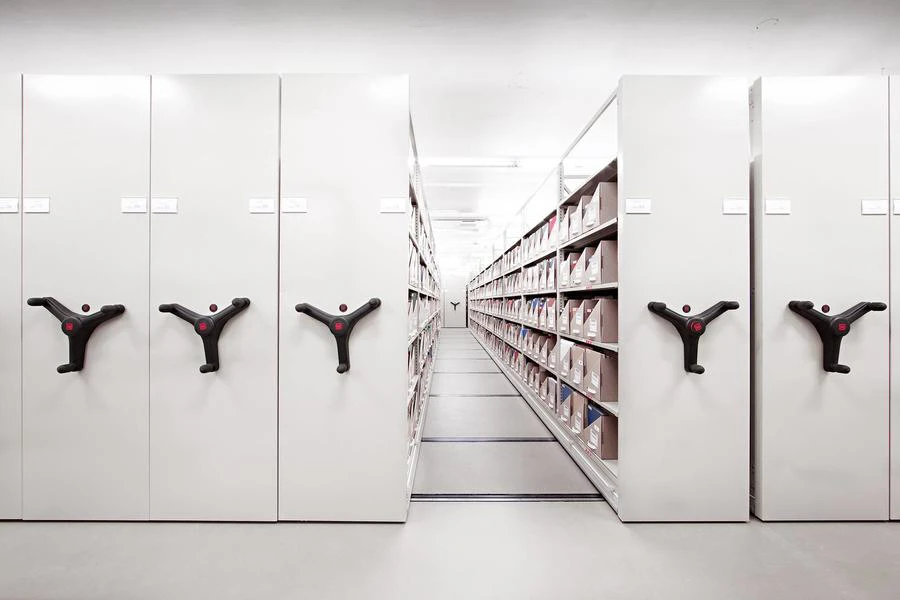
Recognizing the acute commercial need to eliminate static aisle waste, Montel Shelving Inc. engineered its first mechanical-assist mobile storage carriages. By moving entire shelving blocks on heavy-duty precision rails, businesses could halve their required storage footprint.
1980s – 1990sProprietary Patents & Heavy-Duty Mobile Racking
Montel expanded its engineering envelope to include industrial-scale mobile pallet racking, electronic control interfaces, and proprietary safety sweeps. This era established our presence across federal archives, military armories, healthcare campuses, and multinational manufacturing centers.
2000s – 2010sSafeAisle®, SmartShelf® & Museum Innovations
Introduction of the patented SafeAisle® full-floor optical detection system, SafeCrank® ergonomic geared handles, and conservation-grade museum cabinets. Our systems became the gold standard for prestigious cultural institutions, university libraries, and law enforcement evidence repositories.
Present DayLeading Vertical Agriculture & Smart Warehousing
Combining structural expertise with environmental controls, Montel Shelving Inc. has delivered industry-benchmark multi-tier mobile vertical farming systems, clean-room medical carousels, and high-bay mobile racking across the United States, Canada, and global overseas markets.
Our Core Corporate Values
The operational philosophy that guides every engineering calculation, client consultation, and factory build.
Engineering Passion
A relentless pursuit of mechanical perfection and pride in producing storage machinery that performs reliably for decades without compromise.
Continuous Innovation
Constantly optimizing weight distributions, motorized efficiencies, digital safety sweeps, and reduced ecological footprints across our lifecycle.
Customer Centricity
Tailoring every system directly to client-specific SKUs, weight profiles, room heights, seismic codes, and future capacity growth requirements.
Safety & Compliance
Uncompromising adherence to IBC, NBC, ADA, seismic zone ratings, UL/CSA safety certifications, and certified installation standardizations.
Trusted by Global Visionaries & Institutions
Over the decades, premier multinational corporations, Ivy League universities, government agencies, and athletic franchises have entrusted their space optimization to Montel Shelving Inc.
Authorized Distributor Network
Montel Shelving Inc. has cultivated an expansive international network of Authorized Montel Distributors throughout the United States, Canada, Europe, Latin America, and the Middle East. Wherever your project is located, our network provides certified engineering consultation, local code compliance validation, layout design, and factory-trained installation crews.
North American Manufacturing Standards
Every carriage, gear, track, and upright is manufactured in North America under strict quality benchmarks, ensuring immediate replacement parts access, consistent steel gauge integrity, and rapid delivery schedules.
Direct inquiries welcomed for general contractors, architectural specifiers, and procurement officers.
Ready to Optimize Your Facility?
Partner with a century-tested manufacturer. Contact our engineering team for preliminary space calculations, custom 2D/3D BIM layout models, and volume quotation assessments.