Engineered automated warehouse storage and high-density mobile racking solutions optimizing distribution facility square footage
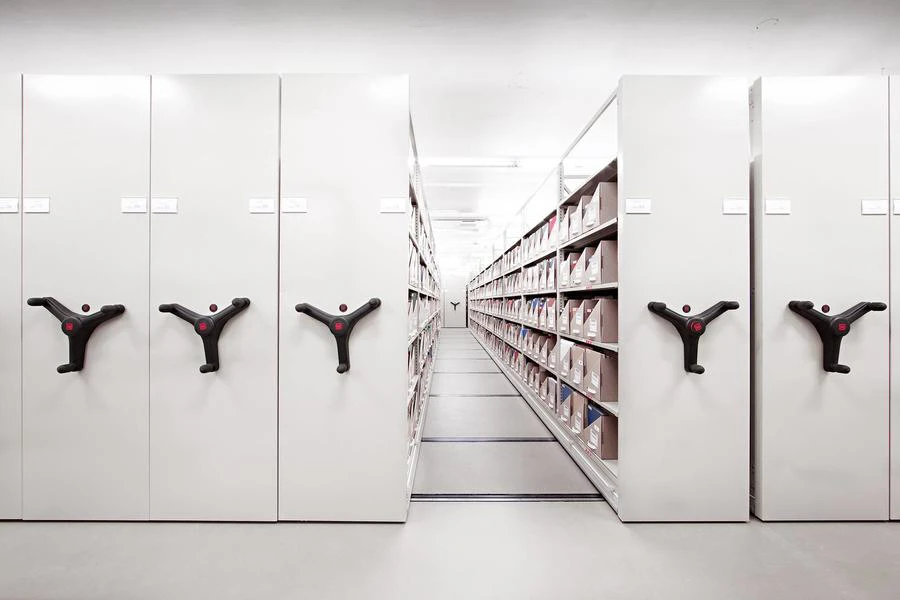
Automated powered mobile storage system compacting warehouse footprint and boosting order picking efficiency
High-density multi-tier industrial racking engineered for precision automated storage
High-Density AS/RS & Powered Mobile Systems · USA & Canada

Automated Warehouse Storage: The Engineering & Procurement Authority

Eliminate static access aisles, double operational cube capacity, and orchestrate zero-downtime logistics with North America's premier automated mobile storage infrastructure.

Up to 50%Reduction in physical warehouse square footage required
100% GainIncrease in usable pallet & SKU storage capacity
100% DutyContinuous automated duty cycle with dual fail-safe sensors
100% NADesigned, manufactured & seismic-certified in North America
Enterprise Product Recommendations

Engineered Automated Warehouse Storage Architectures

Global procurement teams and supply chain engineers face mounting cost pressures per square foot. Discover the high-yield configurations engineered to solve density bottlenecks across heavy pallet, cold storage, and micro-fulfillment environments.

Automated powered mobile pallet racking engineered for industrial distribution warehouses
Heavy-Duty Industrial

Powered Mobile Pallet Racking

Engineered for high-throughput distribution hubs, manufacturing facilities, and freezer vaults. Racking carriages move automatically on embedded steel rails, opening aisles dynamically via WMS commands or radio remote controls to support high-bay reach trucks and AGVs.
Dynamic Pallet LoadWMS IntegratedSafeAisle Sensor System
Multi-tier automated high-density storage shelving with intelligent aisle access controls
Micro-Fulfillment & Parts

High-Bay AS/RS Mobile Shelving

Specialized compact storage for automated order fulfillment, pharmaceutical inventory, MRO tooling, and precision aerospace components. Seamlessly coordinates with autonomous mobile robots (AMRs) and conveyor pick stations to eliminate pick-face travel latency.

High-Density BinsMulti-Tier MezzanineZero-Clearance Drive
Enterprise Engineering & Integrity

Why Montel Shelving Inc. Leads Automated Storage

For decades, Montel Shelving Inc. has engineered high-density mobile racking and automated shelving systems that outperform commodity racking. Here is why Tier-1 North American enterprises trust our turnkey infrastructure.

Engineering leadership icon

Storage-Savvy Engineering

Our structural engineers assess specific floor loads, dynamic carriage torque, and inventory turnover cycles to engineer an automated system tailored specifically to your operation, not an off-the-shelf compromise.

01
Custom configuration icon

Custom Tailored Dimensions

We manufacture one of the most flexible heavy-duty lineups in the logistics sector. Accommodate non-standard pallet depths, high-bay vertical configurations, cantilever racks, or climate-controlled environments with exact precision.

02
SKU management icon

Optimized SKU Organization

Integrate programmable logic controllers (PLCs) with your ERP/WMS to enable automated aisle pre-positioning, night-mode consolidation, fire-aisle opening routines, and secure biometric restricted-access zones.

03
Engineering layout icon

Free FEA & Layout Analysis

Eliminate project risk before issuing capital expenditure approvals. Montel Shelving Inc. provides complete 2D elevation profiles, 3D BIM models, and Finite Element Analysis (FEA) capacity projections at zero cost.

04
Turnkey management icon

Complete Turnkey Execution

Avoid finger-pointing across multiple vendors. From initial floor flatness laser scans and rail installations to heavy carriage fabrication and software integration, one enterprise team guarantees operational excellence.

05
Modular integration icon

Modular Upgrades & Scalability

Our carriages and rail systems feature modular interconnectivity. Start with mechanical-assist or standalone powered units and upgrade to complete WMS-driven automated network configurations as SKU volumes multiply.

06
Patented safety technology icon

Proprietary Patented Safety

Equipped with industry-defining intellectual property including Mobilex®, SafeAisle® full-floor infrared scanning networks, LED Guard® proximity indicators, and SmartShelf® modular load components.

07
North American manufacturing icon

Engineered in North America

Manufactured using North American certified structural steel. Avoid transatlantic shipping backlogs, erratic ocean freight tariffs, and lengthy customs hold-ups while securing verifiable domestic mill test certifications.

08
Logistics delivery icon

Reliable Nationwide Logistics

Our dedicated transport network coordinates direct flatbed delivery and staging across every major freight corridor in the United States and Canada, ensuring seamless project site coordination.

09
Certified installer icon

Certified Precision Installers

Every automated system is assembled and commissioned by factory-certified millwrights and electrical technicians, ensuring tight rail leveling tolerances within 1/16th of an inch across long carriage runs.

10
Space Economics & Volumetric Efficiency

The Engineering Math: Converting Waste Into Usable Cube

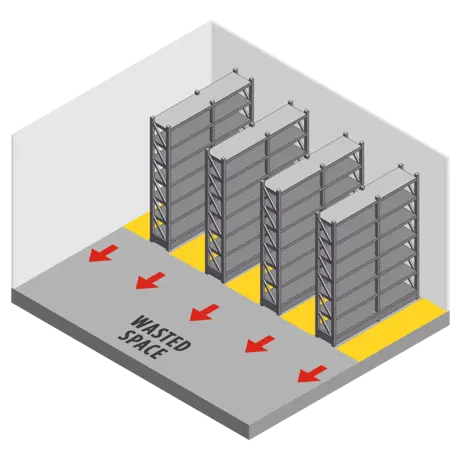
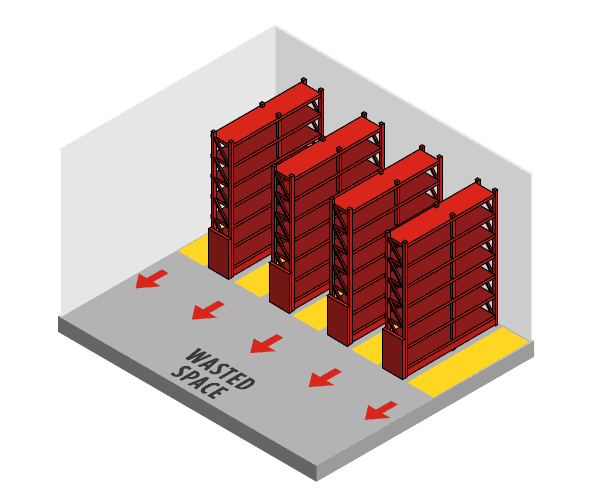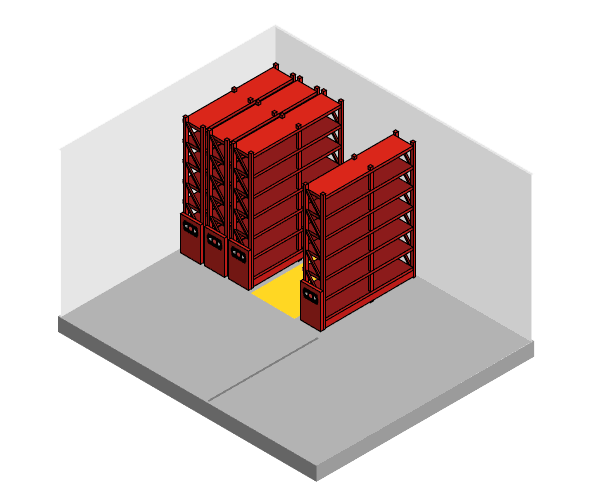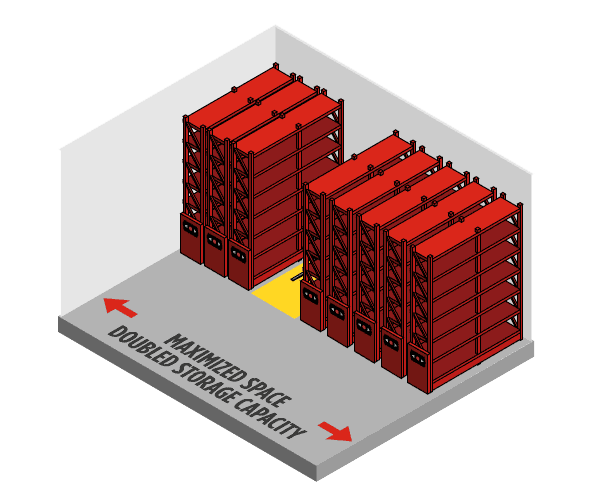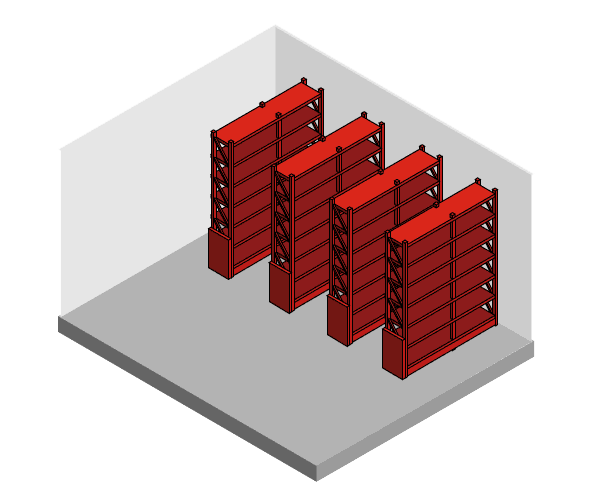
Conventional static warehouse layouts require an access aisle between every two rows of racking, meaning over 50% of the building footprint is paid for yet produces zero revenue. See how automated warehouse storage recovers this space.

Static warehouse layout illustrating empty aisle space requiring heating, cooling, and lighting
Baseline · Static Racking

Wasted Footprint in Fixed Aisles

Static industrial racking dedicates thousands of square feet to permanent access lanes that sit completely empty 90% of the time. Facilities absorb severe real estate overhead, inflated lease rates, and unnecessary utility burdens.

Icon depicting wasted warehouse footprint and unnecessary overhead costs
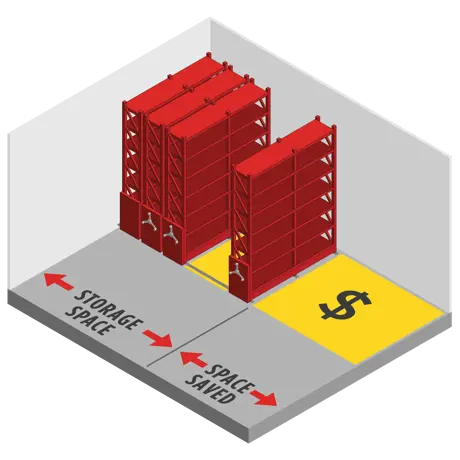
Automated mobile racking condensing warehouse floor space by 50%
Option A · Footprint Reduction

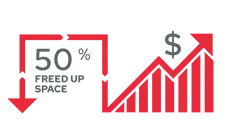
Reclaim 50% Building Floor Space

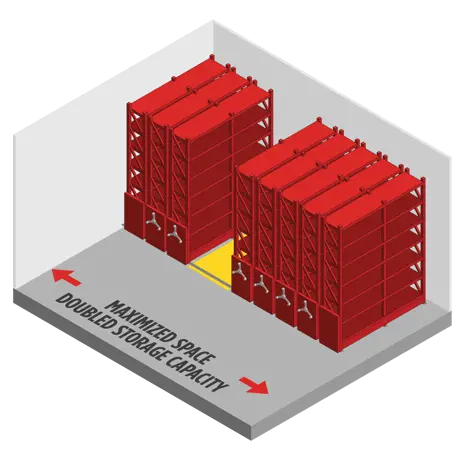
By mounting heavy structural uprights onto motorized automated carriages, entire rows compress into a consolidated high-density storage block. A dynamic aisle opens instantly on demand, liberating floor space for manufacturing and staging lines.

Icon displaying 50 percent floor space freed through mobile racking
High-density mobile storage configuration doubling pallet capacity in existing warehouse
Option B · Capacity Maximization

Gain 100% Greater SKU Density

Retain your current industrial footprint while doubling total storage capacity. Eliminating static access aisles lets you stage twice as many pallet positions in the same building envelope, saving millions in commercial land acquisition.

Icon showing 100 percent increase in storage capacity
Kinematic animation showing mobile storage carriages shifting on precision floor rails to open access aisle
Kinematic Engineering

Dynamic Mobile Aisles: How The Platform Works

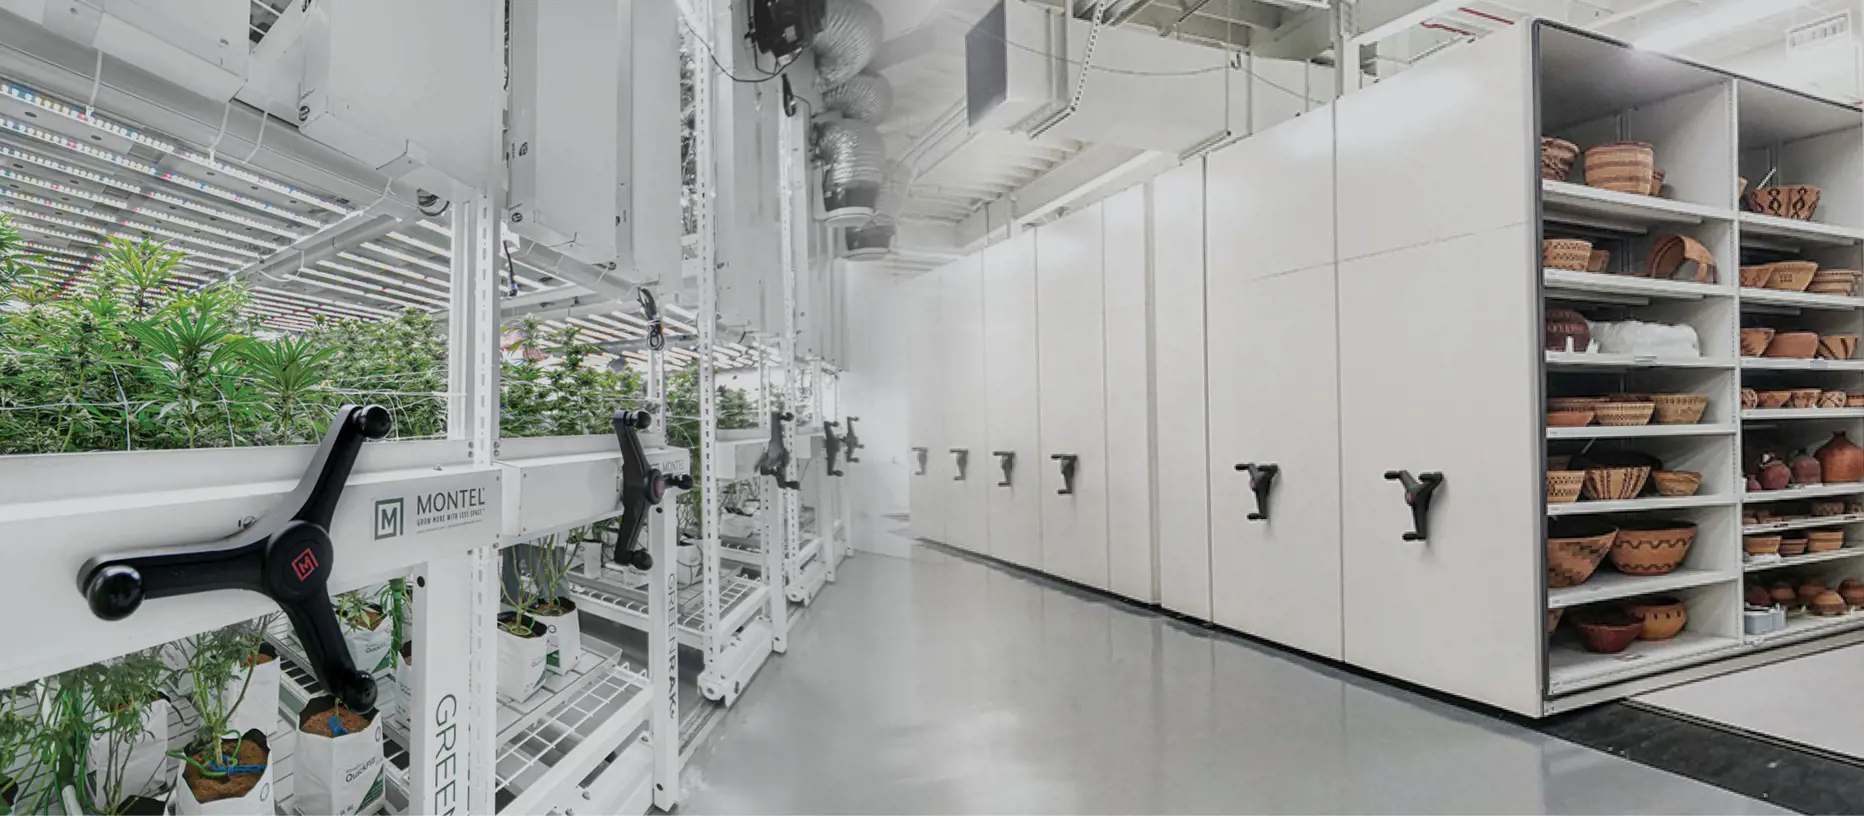
Heavy racking assemblies travel across precision-machined floor rails guided by computer-synchronized AC vector drive motors. Operators and autonomous mobile vehicles trigger aisle selection via WMS API, industrial remotes, or localized touchscreens.

Manual Compact Systems

Ergonomic low-friction mechanical movement for light archival, tooling, and small-parts stockrooms requiring minimal power.

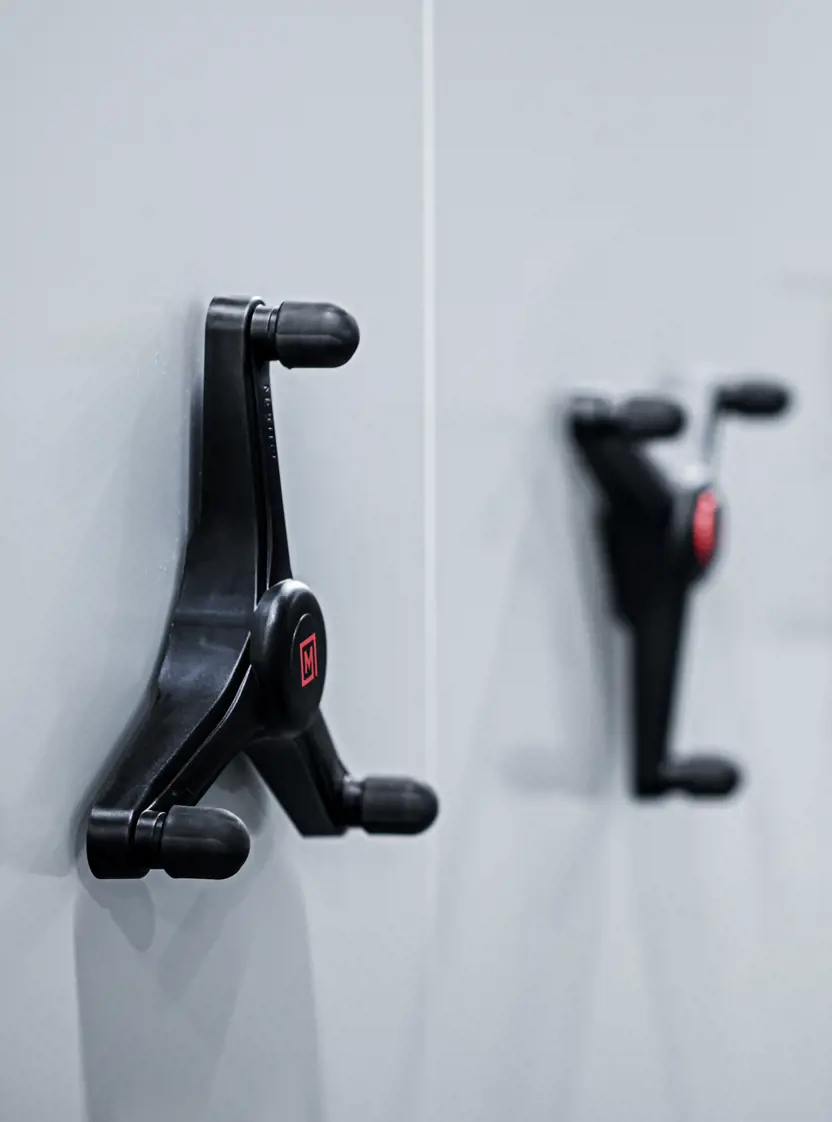
SafeCrank Mechanical-Assist

Patented 3-spoke gear reduction handles allow an operator to move thousands of pounds of inventory effortlessly with single-finger torque.

Fully Automated Powered Execution

Microprocessor-driven automated motion synchronized with warehouse management software, featuring SafeAisle optical safety sweeps and variable-frequency soft-start drives.

Strategic Procurement Horizons

Procurement directors and supply chain VPs face shifting labor dynamics, robotic interoperability requirements, and surging industrial utility rates. Here are the core technical trends driving investments over the next decade.

Trend 01

AMR & AGV Fleet Interoperability

Modern automated warehouse storage is moving beyond human-operated forklifts. Warehouses are deploying autonomous mobile robots (AMRs) that automatically communicate with powered mobile racking. High-speed optical bus lines and RESTful APIs pre-open picking aisles as the AMR approaches, eliminating cycle wait times and boosting pick throughput up to 300%.

Trend 02

AI Predictive Slotting & Balancing

Procurement specifications now frequently mandate AI-driven slotting integration. Machine learning algorithms analyze seasonal SKU velocity, order groupings, and center-of-gravity load distributions. The automated racking controller shifts overnight to position the day's highest-velocity inventory for immediate access, reducing carriage transit time.

Trend 03

Decarbonization & Cold Chain ROI

Refrigerated warehouse facilities consume substantial energy just maintaining sub-zero cubic volume. By compacting pallet storage and eliminating 50% of wasted aisle air space, automated mobile racking slashes thermal loss and refrigeration energy loads by 40% to 50%, speeding up carbon-neutral compliance and yielding immediate utility savings.

Trend 04

Seismic Resilience & Micro-Tolerances

With distribution centers locating closer to major coastal metro areas subject to IBC seismic performance categories D through F, procurement demands advanced structural dampening. Montel Shelving Inc. engineers carriages with continuous anti-tip guides, dual-rail anchors, and torsional stiffness that withstand ground acceleration while maintaining rack alignment.

Trend 05

Retrofit-Friendly Surface-Mount Rails

Supply chain leaders increasingly avoid long warehouse greenfield development cycles. The newest procurement trend prioritizes high-density automated racking that mounts over existing concrete slabs using low-profile surface rails and modular decking ramps, avoiding destructive concrete trenching and shortening project commissioning by months.

Trend 06

Full-Spectrum Safety & Zero-Liability

Human-robot collaborative workspaces require fail-safe safety standards. Next-generation automated warehouse storage features overlapping safety curtains, multi-zone infrared sweeps, and dynamic zero-touch deceleration. Carriages halt immediately if a misplaced pallet or technician breaches an aisle, protecting employees and sensitive inventory.

Industry Specific Deployments

Engineered For Specialized Industrial Sectors

Explore how Montel Shelving Inc. delivers space-doubling automated storage infrastructure across diverse commercial, industrial, and institutional supply chains.

Athletics equipment storage icon

Athletics Logistics

Athletics Logistics

High-density automated gear lockers, team equipment storage, and uniform vaults for universities and professional sports complexes.

Automotive and aerospace components icon

Automotive & Aerospace

Automotive & Aerospace

Engineered automated tire racking, heavy die storage, turbine blade vaults, and MRO manufacturing inventory racks.

Healthcare medical inventory icon

Healthcare & Pharma

Healthcare & Pharma

Automated pharmaceutical vaults, sterile supply centers, medical records storage, and temperature-controlled sample preservation.

Food processing and cold storage icon

Cold Chain & Freezer

Cold Chain & Freezer

Heavy-duty refrigerated automated mobile pallet racking designed for sub-zero freezer environments down to -30°C.

Retail omnichannel fulfillment icon

Retail Fulfillment

Retail Fulfillment

Back-of-house automated storage, e-commerce mini-load fulfillment, and high-security luxury retail inventory vaults.

Library high-density archival icon

Library & Archival

Library & Archival

Automated compact book repositories, off-site university storage depositories, and climate-controlled rare manuscript vaults.

Education campus storage icon

Education Campuses

Education Campuses

Centralized facilities management storage, laboratory research inventory, and institutional athletic equipment rooms.

Military secure armory storage icon

Defense & Armories

Defense & Armories

High-security automated weapon racks, tactical gear lockers, sensitive optics storage, and parachute deployment systems.

Public safety evidence storage icon

Public Safety Evidence

Public Safety Evidence

Secure audit-trailed evidence storage, chain-of-custody lockers, and precinct supply mobile shelving.

Museum art collection storage icon

Museum Fine Arts

Museum Fine Arts

Automated pull-out painting screens, conservation-grade textile flat files, and modular artifact storage cabinets.

Industrial warehouse distribution icon

Distribution Centers

Distribution Centers

Heavy pallet mobile racking, high-bay carton AS/RS systems, staging buffers, and raw materials staging racks.

Government agency archive icon

Government Agencies

Government Agencies

Classified municipal, state, and federal archive vaults, IT equipment staging, and judicial records management.

Automated garage and residential storage icon

Specialty Residential

Specialty Residential

Collector automotive racking, luxury estate wine vaults, and ski/gear storage systems for premier developments.

Explore All Sectors

View technical engineering submittals and certified load case studies across North American markets.

Engineering Governance & Standards

Technical Standards for North American Installations

Procuring automated warehouse storage requires compliance with structural safety, electrical reliability, and fire prevention mandates. Montel Shelving Inc. systems meet or exceed all North American regulatory standards.

Seismic Category A–F Compliance

Engineered anti-tip brackets and ductile steel carriages satisfy rigorous International Building Code (IBC) and NBCC seismic force requirements, ensuring safe structural behavior in active seismic regions.

Precision Slabs & Laser Alignment

Carriage rails are leveled with high-precision laser optical instruments to tight tolerances, ensuring smooth carriage travel, eliminating dynamic load shifting, and preventing wheel binding.

NFPA 13 Fire Protection Clearance

Carriage controllers support automated open-spread modes upon receiving building fire alarm signals, enabling uniform overhead sprinkler water penetration across every storage level.

LEED v4 & Environmental Stewardship

High-recycled-content North American steel, low-VOC powder coat finishes, and energy-efficient programmable sleep circuits support enterprise ESG disclosures and LEED green building certification.

Parametric Revit / BIM Documentation

Our engineering support department provides native Autodesk Revit and CAD assets, enabling project architects and structural engineers to drop fully parametric assemblies directly into master models.

Factory-Trained Millwrights

From initial concrete moisture testing and laser-guided rail anchoring to control panel PLC programming, factory-certified technicians manage every step of system installation.

Building code parameters and floor capacity criteria vary by jurisdiction. Montel Shelving Inc. works with your structural engineering team and local building officials to confirm all requirements.

Enterprise Procurement FAQ

Answers to Global Buyer & AI Search Inquiries

Detailed engineering, economic, and technical answers addressing the key questions global supply chain directors, industrial architects, and purchasing teams ask before investing in automated warehouse storage.

Get a Quote
How does automated warehouse storage reduce industrial footprint requirements by 50%?
Conventional static warehouse racking requires a dedicated aisle for every two storage faces, consuming up to 60% of floor space purely for vehicle movement. Automated warehouse storage and powered mobile racking systems eliminate these static aisles by mounting heavy-duty shelving units on electronically synchronized carriages running on flush or low-profile floor rails. An automated aisle opens on demand via software, radio frequency (RF), or touch interface, condensing storage density and slashing footprint requirements by 50% while doubling inventory capacity within existing architectural envelopes.
Can automated mobile racking systems be integrated into existing concrete slabs without structural trenching?
Yes. Engineered modular low-profile surface-mount rail networks with ramp transitions allow automated mobile storage to be installed directly on existing industrial concrete floors without structural saw-cutting or foundation trenching. For new builds or heavy industrial pallet operations, flush recessed rails can be embedded during construction, engineered to support concentrated axle loads while maintaining zero-barrier forklift and automated guided vehicle (AGV) transit.
What safety systems protect personnel and automated machinery within powered mobile aisles?
Advanced automated storage systems incorporate multi-tiered fail-safe safety ecosystems. These include patented infrared floor-level sweep sensors (such as SafeAisle technology), photoelectric entry beams, torque-limiting dynamic drive brakes, mechanical contact bars, and emergency stop circuits. If an operator, forklift, or dropped inventory disrupts a light curtain or sweep field, carriage motion instantly locks down with electronic dynamic braking to prevent damage or injury.
How do automated warehouse storage systems withstand seismic and high-load dynamic stresses?
Industrial automated storage units engineered by Montel Shelving Inc. utilize heavy-gauge structural steel carriages equipped with patented anti-tip rail systems, dual-flange steel wheels, and anchor brackets engineered to comply with strict International Building Code (IBC) and National Building Code of Canada (NBCC) seismic standards across all seismic performance categories (A through F).
What is the typical Return on Investment (ROI) and total cost of ownership (TCO) timeline for automated warehouse storage?
Most enterprise facilities achieve complete capital expenditure payback within 14 to 28 months. ROI is driven by avoiding expensive facility expansion or off-site warehouse leases, reducing refrigeration energy consumption by up to 50% in temperature-controlled cold chains, lowering HVAC lighting overhead, and reducing human transit and picking times by 40% to 65%.
How does automated mobile racking integrate with Warehouse Management Systems (WMS) and Autonomous Mobile Robots (AMRs)?
Modern automated storage platforms feature open industrial architecture (EtherNet/IP, Modbus TCP, RESTful APIs) allowing direct bidirectional communication with enterprise WMS and ERP software. When a picking wave is initiated, the WMS signals the racking controller to pre-open the designated storage aisle automatically before an AMR or order picker arrives, eliminating cycle wait times.
High-Density Space Feasibility Analysis

Plan Your Automated Storage Project With Montel Shelving Inc.

Submit your project footprint, clear ceiling height, and inventory load specifications. Our engineering team will produce a comprehensive 2D/3D capacity study detailing the square footage you can recover.

FootprintFloor dimensions & clear height
Capacity TargetPallet or SKU counts
PayloadUnit loads & rack weights
Automation TypePowered electrical or automated AS/RS
LocationUnited States or Canada
Engineering ScopeCAD, Revit, FEA & seismic review
Automated powered mobile storage carriage drive and control system manufactured by Montel Shelving Inc.
Precision Automated Carriage Engineering High-torque drive motors, dual optical safety sweeps, and heavy-gauge North American structural steel built for 24/7 industrial logistics.