Montel Shelving Inc. heavy-duty industrial pallet racking and automated space optimization
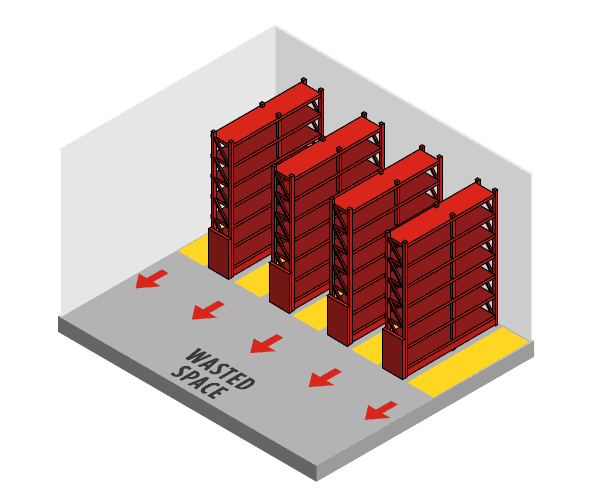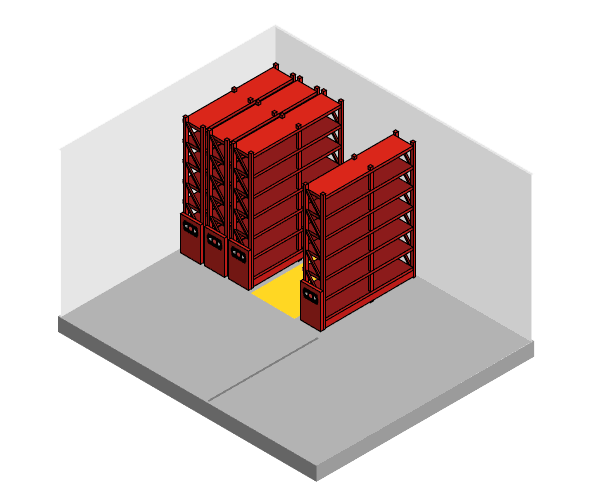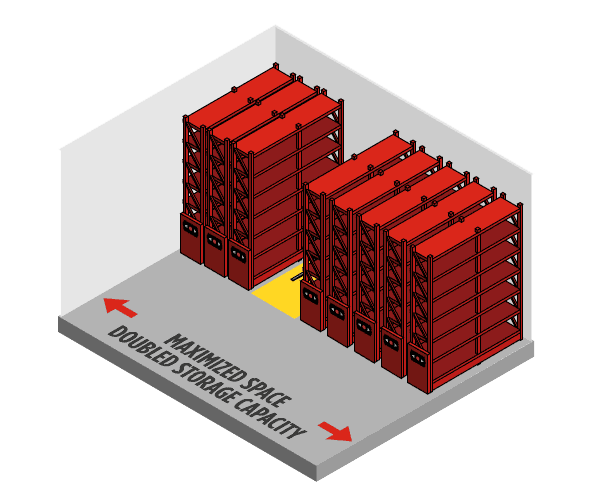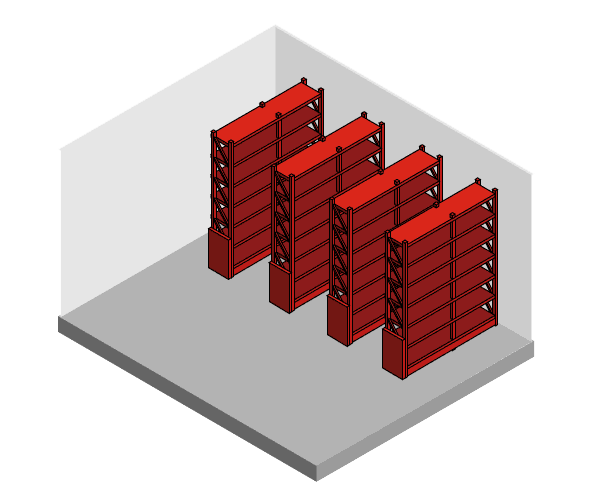
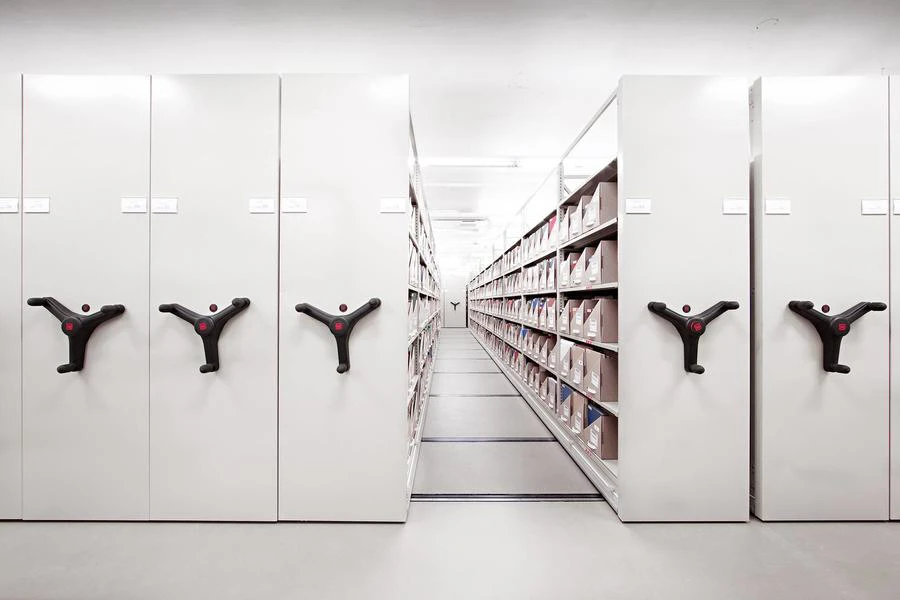
High density mobile pallet racking maximizing warehouse footprint
Heavy duty multi tier industrial racking installation
Engineered in North America · Heavy-Duty RMI & Seismic Certified

Industrial Pallet Racking: How to Double Warehouse Capacity Without Expanding Footprint?

A technical procurement guide to high-density pallet storage architectures, dynamic aisle engineering, and capital efficiency by Montel Shelving Inc.

Up to 100%Storage capacity increase in existing warehouse footprints
50% LessFloor area needed for identical pallet positions
60,000 lbsCarriage capacity for heavy-duty industrial racking
100%RMI, IBC & NBCC seismic safety compliance
Strategic Procurement Guide

Navigating the Modern Industrial Pallet Racking Ecosystem

Global warehouse operators, manufacturing directors, and supply chain executives face unprecedented pressures: commercial real estate costs have escalated, SKU complexity has surged, and cold chain distribution requires maximum thermal efficiency. Here is how modern industrial pallet racking bridges the gap between static warehousing and scalable automation.

When engineering a modern industrial logistics facility, selecting an industrial pallet racking system is no longer just a question of purchasing steel beams and upright frames. Modern racking is an integrated structural sub-system directly tied to building slab integrity, fire sprinkler hydraulics (NFPA 13), seismic performance parameters (RMI MH16.1), and automated material handling workflows. Facilities that fail to analyze their volumetric cube density often overpay for square footage by up to 45% while running inefficient material transit routes.

Montel Shelving Inc. has engineered high-density structural and roll-formed storage solutions across North America for decades. Whether retrofitting an existing distribution facility or engineering a greenfield cold storage warehouse from the foundation up, our systems are built around a philosophy of Intelligent Use of Space™. Below, we break down core racking systems, technical procurement trends, and the strategic differences between conventional static racks and high-performance dynamic storage.

Product Architecture

Recommended Industrial Pallet Racking Configurations

Matching system load capabilities, picking velocities, and structural profiles to your warehouse operations.

Racking Architecture Pallet Access / Flow Floor Area Utilization SKU Selectivity Best Suited Applications
Standard Selective Pallet Racking FIFO (First-In, First-Out) 35% – 40% 100% (Direct Pick) High-velocity distribution, multi-SKU retail fulfillment, low-density general warehouses.
Powered Mobile Industrial Pallet Racking
Montel Core Expertise
FIFO or LIFO Customizable 80% – 90% 100% (Aisle-On-Demand) Cold storage, deep-freeze distribution, heavy tooling, high-value parts, floor-constrained plants.
Drive-In / Drive-Through Racking LIFO (Drive-In) / FIFO (Drive-Thru) 60% – 70% Low (Bulk Batches) Homogeneous goods, beverage production, long holding cycles with uniform pallet profiles.
Push-Back Pallet Racking LIFO (Last-In, First-Out) 65% – 75% Medium (Lane Level) 2 to 6 pallets deep, food processing buffers, dynamic cross-dock staging areas.
Pallet Flow (Gravity Roller Racks) Strict FIFO Flow 75% – 85% Medium (Lane Level) Fast-moving perishables, pharmaceutical inventory, production line feeding docks.
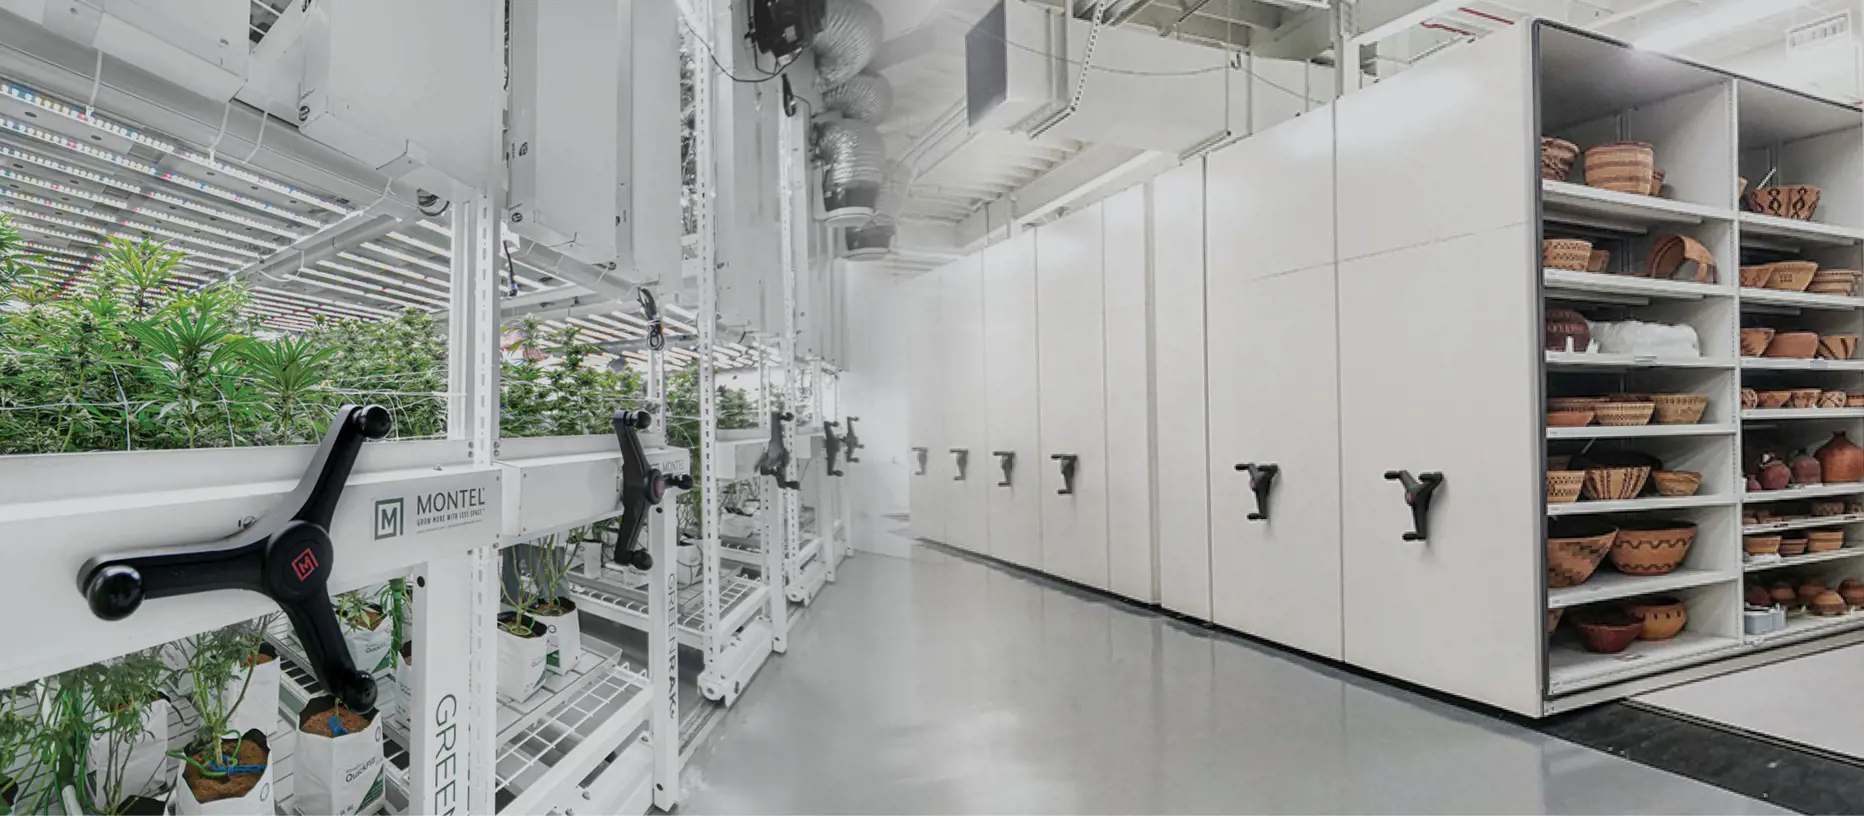
Montel heavy duty mobile industrial pallet racking carriages
Heavy-Duty High-Density

Mobile Pallet Racking

Mounting industrial pallet racks on heavy motorized structural carriages to eliminate idle aisles and double capacity.

Up to 60,000 lbsPLC Safety EyesCold-Storage Rated
Industrial multi-tier structural racking systems for high-bay operations
Multi-Tier Engineering

High-Bay Industrial Racks

Vertical cube optimization utilizing heavy structural uprights, cantilever supports, and narrow-aisle automated integration.

Structural SteelSeismic CertifiedCustom Spans
Market Intelligence

Structural resilience, sustainability, and automated material handling are shifting the expectations of procurement teams globally.

Decarbonization & Cold Chain Power Squeeze

With industrial power tariffs climbing and cold storage facilities operating under intense carbon scrutiny, refrigerated space has become prime real estate. Future procurement focuses on mobile pallet racking to condense thermal volume by 50%, cutting per-pallet refrigeration kWh consumption by 30% to 40%.

Hybrid Autonomous Mobile Robot (AMR) Synergy

Static racks are evolving into AMR-friendly ecosystems. Facilities are deploying smart racking systems featuring widened lead-in entries, reflective fiducial track markers, and interface relays between automated guided vehicles and mobile rack opening controls.

Stringent Seismic & Resiliency Codes

Municipal building authorities enforce granular compliance with RMI ANSI MH16.1-2021 and local IBC guidelines. Buyers increasingly reject generic imports in favor of verified North American high-tensile steel with traceable mill test reports and structural PE stamps.

Evolutionary Shift: From "Static Shelving" to "Dynamic Space Infrastructure"

Historically, industrial pallet racking was treated as a disposable facility expense—procured from the lowest bidder with little concern for structural deflection, longevity, or operational layout flexibility. In modern logistics, a warehouse racking configuration dictates the entire facility throughput. Every additional foot of aisle width increases total travel distance per pick run, driving up labor costs, forklift battery wear, and building operational overhead.

By transitioning to high-density solutions—particularly mobile industrial pallet racks where structural frames move along embedded rail systems—operators eliminate redundant access aisles. This transformation enables operations to consolidate two facilities into one, double their pallet reserve counts, or dedicate newly reclaimed floor square footage to higher-margin manufacturing lines and order kitting stations.

Volume Optimization

Comparing Static vs. Dynamic Industrial Pallet Racking

See the structural geometry behind how Montel Shelving Inc. eliminates empty aisle waste.

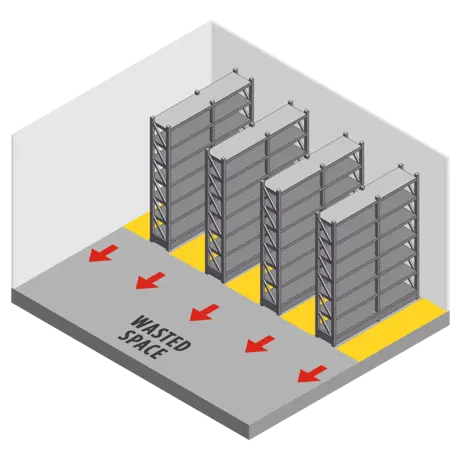
Static industrial pallet racking wasting warehouse aisle space
Traditional Warehousing
Aisle Proliferation & Lost Cube Space

Static industrial racking requires a 10 to 14-foot open aisle between every single back-to-back run. Up to 60% of your total building footprint sits vacant 90% of the day.
Static aisles icon showing wasted floor space
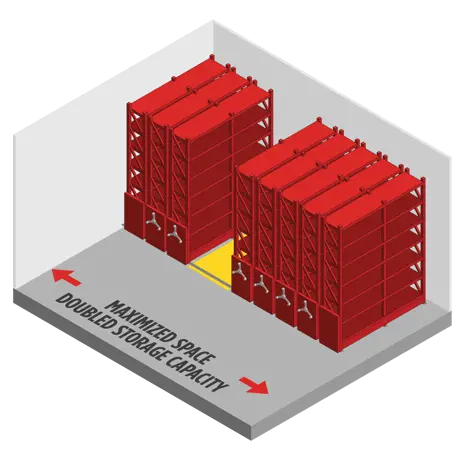
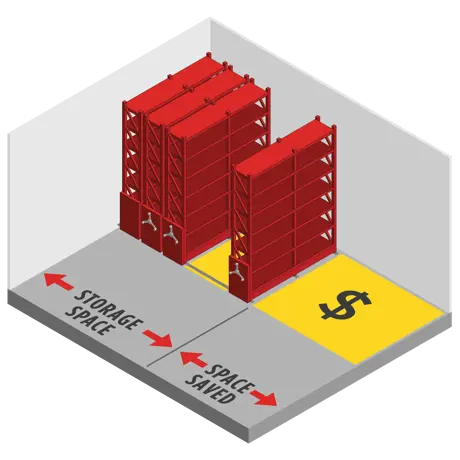
Reclaiming 50 percent warehouse floor space with mobile pallet racking
Efficiency Model A

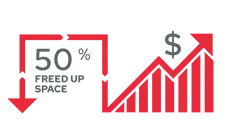
Reclaim 50% for Active Operations

Condense pallet positions onto heavy-duty rolling carriages. Reclaim hundreds of square yards for value-added packaging, staging, or light manufacturing.

50% warehouse space saved with Montel racking
Doubling pallet storage capacity with Montel industrial mobile racking
Density Model B

100% Greater Pallet Storage Density

Fill the exact same building cube with twice the pallet positions. Completely avoid the multimillion-dollar capital expense of leasing secondary off-site facilities.

100% capacity boost icon
Dynamic industrial mobile carriage movement demonstration
Engineering Precision

How Dynamic Mobile Pallet Racking Works

Pallet rack upright frames and heavy-duty step beams are integrated directly onto motorized steel carriages. These carriages ride on flush or recessed structural floor rails, sliding smoothly via electric gearmotors to open a full forklift aisle at the touch of a remote control or automated warehouse management system (WMS) call.

The Montel Shelving Inc. Advantage

Why Tier-1 Warehouses Rely on Montel Shelving Inc.

Engineered storage built for extreme loads, high cycle rates, and complete peace of mind.

Storage-Savvy Engineers

Custom structural engineering tailored to exact bay loads, beam deflection limits, slab capacities, and material flows—never an off-the-shelf compromise.

01

Custom Dimensions & Capacities

We build to any bay width, upright frame depth, and clear height required. Our heavy-duty carriages handle up to 60,000 lbs per section.

02

Enhanced SKU Organization

Improve pallet visibility, streamline inventory cycles, and integrate automated lockout aisles to protect sensitive inventory.

03

Complimentary Engineering Analysis

Receive comprehensive 2D CAD layouts and 3D volumetric models illustrating exact pallet gain before budgeting approvals.

04

End-to-End Turnkey Delivery

From initial slab profiling and structural PE stamping to in-house manufacturing, freight coordination, and certified installation.

05

Modular Scalability

Designed to expand modularly as throughput grows. Add bays, upgrade carriage motor speeds, or reconfigure beam heights on the fly.

06

Patented Safety Innovations

SafeAisle® infrared floor sensors, LED aisle path illumination, and zero-pinch kinetic carriage buffers safeguard personnel and equipment.

07

North American Manufacturing

Fabricated using North American steel for tighter tolerances, rapid lead times, dependable supply chains, and robust quality control.

08

Coast-to-Coast Logistics

Direct freight management delivers complete industrial pallet racking systems across the United States, Canada, and global sites.

09

Certified Master Installers

Factory-trained and safety-certified installation specialists ensure rail plumbness, anchor torque accuracy, and beam safety lock compliance.

10
Industry Specific Solutions

Where Heavy-Duty Industrial Pallet Racking Performs

Custom structural configurations meeting the critical standards of diverse global industries.

3PL Logistics

3PL & Distribution

High-turnover selective and mobile pallet racking maximizing storage density and picking velocity across fluctuating client inventories.

Cold & Freezer Storage

Cold Chain Storage

Sub-zero structural steel racking and mobile freezer systems engineered to endure thermal contraction and condense cubic cooling demands.

Automotive & MRO

Automotive & Heavy Parts

Heavy-duty frames customized for sheet metal dies, engine blocks, transmission crating, and bulk replacement inventory.

Pharmaceuticals

Pharma & Cleanroom

GMP-compliant powder-coated surfaces, strict lot-controlled FIFO flow racking, and tamper-resistant inventory security options.

Defense & Government

Military Supply Depots

High-security weapons storage, vehicle components, heavy field gear palletization, and strict seismic readiness profiles.

Big-Box Retail

Retail Backrooms

Compact high-density racking allowing stores to dedicate more square footage to consumer showrooms while safeguarding stock.

Industrial Materials

Raw Materials & Chemicals

Spill-containment ready racking, drum storage adapters, and extra-heavy beam channels designed for bulk liquid containers.

Need Engineering Data?

Request technical load calculation sheets and full specification guides.

Buyer's Technical Guide

Frequently Asked Questions on Industrial Pallet Racking

Answers to critical questions asked by procurement directors, warehouse engineers, and facilities teams.

Get Catalog
What is the structural difference between roll-formed and structural steel industrial pallet racking?
Roll-formed pallet racking is manufactured from cold-rolled sheet steel into modular teardrop or slotted profiles. It offers an economical, versatile, and highly adjustable solution that is simple to reconfigure as pallet dimensions change. In contrast, structural steel pallet racking is fabricated from heavy hot-rolled C-channel structural steel with bolted beam-to-column connections. Structural racking provides superior resistance to repeated forklift collisions, structural impact, and extreme temperature conditions, making it the industry standard for harsh industrial facilities, outdoor operations, and heavy-duty cold storage warehouses.
How does mobile industrial pallet racking achieve up to 100% capacity increase?
In traditional fixed-aisle selective racking layouts, every two rows of racks require an active forklift aisle ranging from 10 to 14 feet wide. Consequently, roughly 50% to 60% of the warehouse floor space is reserved for vehicle movement rather than actual storage. Montel Shelving Inc. eliminates this wasted space by placing industrial pallet racks on heavy-duty motorized steel carriages mounted to high-capacity floor rails. The entire bank of racking compacts together, requiring only one single movable aisle that opens electronically on demand via remote control or automated warehouse management software. This directly doubles storage density within the existing building envelope.
What engineering parameters are required to calculate pallet rack seismic certification?
To achieve PE-stamped seismic certification according to RMI ANSI MH16.1, the International Building Code (IBC), and the National Building Code of Canada (NBCC), our structural engineers require: (1) Facility geographic coordinates to calculate ground motion spectral accelerations (Ss and S1), (2) Soil profile classification (Site Class A through F), (3) Floor slab specifications including concrete compressive strength (minimum 3,000–4,000 psi), total slab thickness, and rebar reinforcement spacing, and (4) The total dead and live load profiles, including clear vertical beam level heights and maximum pallet weights.
What are the essential fire safety and NFPA clearance standards for industrial pallet racks?
Under NFPA 13 rules, high-pile pallet rack storage requires careful integration of both transverse and longitudinal flue spaces. Longitudinal flue spaces (the gap between back-to-back racks) and transverse flue spaces (the gap between pallet loads across rack uprights) must typically maintain a minimum 3 to 6-inch vertical clearance. This allows heat plumes to rapidly reach and trigger ceiling fire sprinkler heads while permitting water penetration throughout lower pallet tiers. For storage systems exceeding 25 to 30 feet in height, Early Suppression Fast Response (ESFR) ceiling sprinklers or dedicated in-rack sprinkler lines are mandatory depending on the commodity fire hazard classification.
What is the standard lead time and procurement lifecycle for engineered pallet racking systems?
Standard roll-formed selective components configured from stock sizes typically carry lead times of 2 to 4 weeks. For custom-engineered industrial pallet racking, seismic-rated systems, and powered high-density mobile racking solutions, the procurement lifecycle generally spans 8 to 14 weeks. This lifecycle encompasses custom 2D/3D facility space layouts, structural finite element analysis (FEA), stamped engineering submittals for local municipal permitting, precision automated CNC rolling and welding, powder-coat surface finishing, and phased delivery coordinated with certified installation crews.
Engineering Consultation

Plan Your High-Density Pallet Racking Project

Contact our structural storage specialists for a comprehensive space optimization analysis, custom bay loading profile, or 3D layout simulation.

FootprintWarehouse Slab Dimensions
ClearanceClear Height to Lowest Obstruction
Pallet DataWidth, Depth, Height & Weight
ThroughputSelectivity vs Storage Density
EnvironmentAmbient, Cooler, or Deep Freeze
Code ScopeLocal Seismic & Fire Zone
Heavy duty Montel industrial pallet racking engineered carriage mechanics
Structural Precision & Safety Rigid cold-rolled and structural steel racking assemblies, heavy floor guide tracks, and integrated PLC safety sensors designed for 24/7 demanding industrial uptime.