Why Global Leaders Choose Our Storage Systems
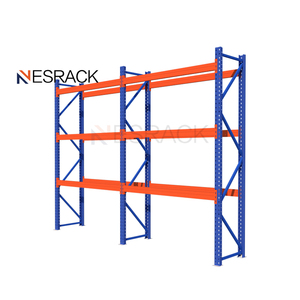
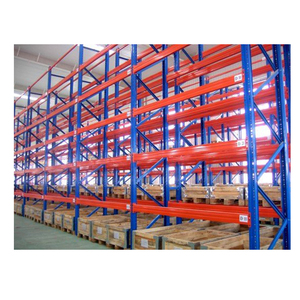
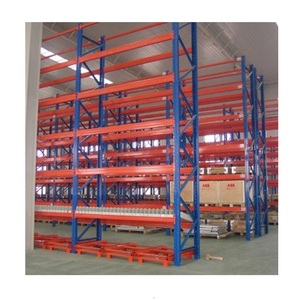
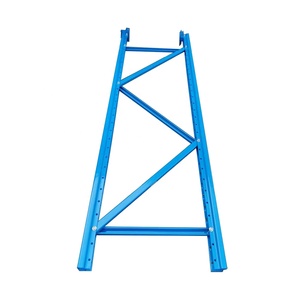
In the evolving landscape of global logistics, our CE Certified Industrial Storage Racks represent the intersection of safety and structural efficiency. Unlike standard market offerings, our racks are engineered to meet stringent EU safety standards, ensuring that every boltless connection and upright frame offers maximum load-bearing reliability.
Our commitment to Information Gain ensures that we don't just sell shelves; we provide a consultative approach to warehouse space optimization. By analyzing SKU density, forklift turn radii, and load-bearing requirements, we transform your facility into a high-performance distribution hub.
Industry Trends & Future Outlook
The transition toward Automated Storage and Retrieval Systems (AS/RS) is shaping the next decade. Our current generation of steel pallet racks is designed with the precision tolerances required for automated crane interaction. Furthermore, sustainability is becoming a key purchase driver; our powder-coating processes minimize VOC emissions, aligning with global green building initiatives.
Frequently Asked Questions
What does CE certification mean for my warehouse?
CE marking confirms that our products meet the European Union's safety, health, and environmental requirements, providing a globally recognized benchmark for structural integrity and quality control.
How do I determine the right rack load capacity?
We provide a comprehensive load-bearing calculation based on your specific pallet weights and beam lengths. Always factor in the maximum pallet weight and safety margins for seismic risks.
Is custom sizing available?
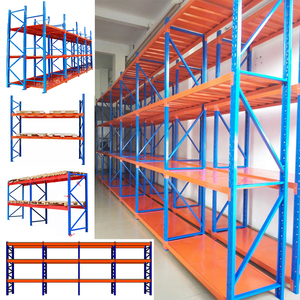
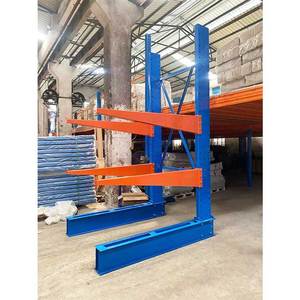
Yes. As a direct manufacturer, we provide bespoke heights, beam widths, and powder-coating colors to fit unique warehouse footprints.