Dispensing Density
Central Hospital Pharmacies
High-density mechanical-assist and motorized mobile shelving designed for high-turnover unit-dose bottles, IV bags, and bulk pharmaceutical inventory.
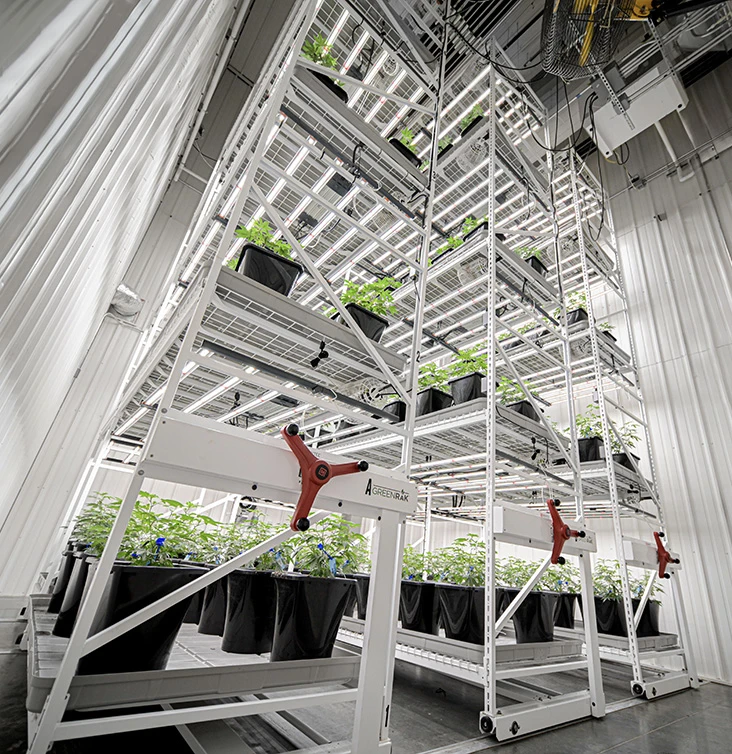
Double pharmaceutical stock capacity in your central dispensary while cutting picking travel time in half. Engineered by Montel Shelving Inc. for error-free medication management.
Modern pharmaceutical environments face unprecedented challenges: expanding specialty medication formularies, strict cold-chain and cleanroom mandates, automated robotic replenishment, and escalating real estate costs. Here is how modern high-density pharmacy storage systems transform clinical facilities.
High-density mechanical-assist and motorized mobile shelving designed for high-turnover unit-dose bottles, IV bags, and bulk pharmaceutical inventory.
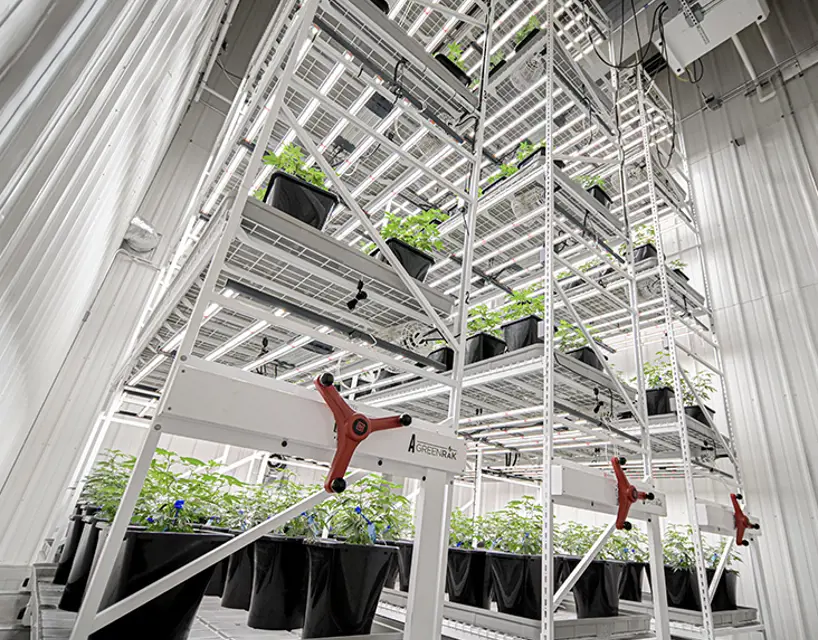
Controlled drug containment and buffer-zone cleanroom storage systems with non-outgassing finishes, laminar air-flow compatibility, and biometric access.
Select the ideal architectural shelving configuration built around specific clinical workflows, weight requirements, and sanitary regulations.
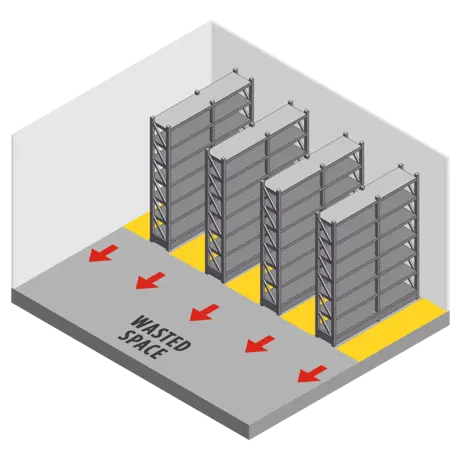
Equipped with our patented SafeCrank™ gear-reduction mechanism, this system enables pharmacy technicians to move thousands of pounds of oral solids, injectables, and bulk IV fluids effortlessly with minimal rotational push.
Designed for Schedule II controlled substances and high-value oncology medications. Features full-floor infrared safety sweeping sensors, programmable PIN keypad access, and audit trail integration with hospital building security.
Specifically manufactured for negative and positive pressure cleanroom suites. Solid stainless-steel or electro-galvanized non-porous powder coating resists frequent hospital chemical wipes, bleach disinfectants, and quaternary ammonia solutions.
For decades, Montel Shelving Inc. has engineered durable, space-reclaiming high-density systems across North America. Our client-first manufacturing standards set the benchmark in healthcare storage precision.

Every pharmacy configuration is engineered around medication turnover rates, narcotic security mandates, and cleanroom air balances—not generic retail dimensions.
01
Custom carriage widths, depths, and heights allow acute care hospital pharmacies to maximize clear ceiling height and fit around structural columns.
02
Integrated angled medication trays, divider bins, and label channels ensure high-alert medications remain isolated, preventing dispensing errors.
03
Receive comprehensive 2D CAD elevation plans, BIM/Revit models, and 3D walkthrough layouts to visualize capacity gains before purchasing.
04
Montel Shelving Inc. oversees structural floor engineering, manufacturing, delivery, assembly, and commissioning under single-source accountability.
05
Add refrigerated drug lockers, hanging IV bar racks, and modular pull-out drawers as clinical formularies grow over the next decade.
06
Patented SafeAisle® infrared floor sensors and LED Guard™ automatically detect personnel and carts inside an open aisle, halting movement instantly.
07
Manufactured using robust structural steel in North America, delivering unmatched mechanical durability, shorter lead times, and rigorous ISO quality control.
08
Coordinated logistics deliver turnkey medical and pharmacy shelving packages across the United States, Canada, and global healthcare facilities.
09
Installed by factory-trained technicians experienced in sensitive hospital working environments, infection control, and seismic building codes.
10As healthcare systems transition toward centralized distribution models and automation, medical storage architecture is evolving rapidly. Stay ahead of regulatory and operational demands by understanding key procurement vectors.
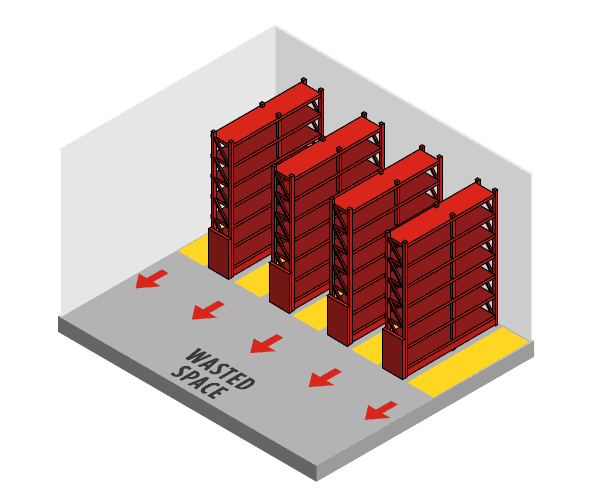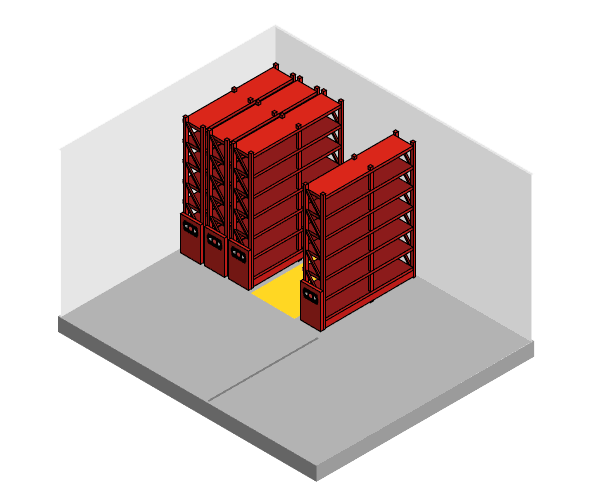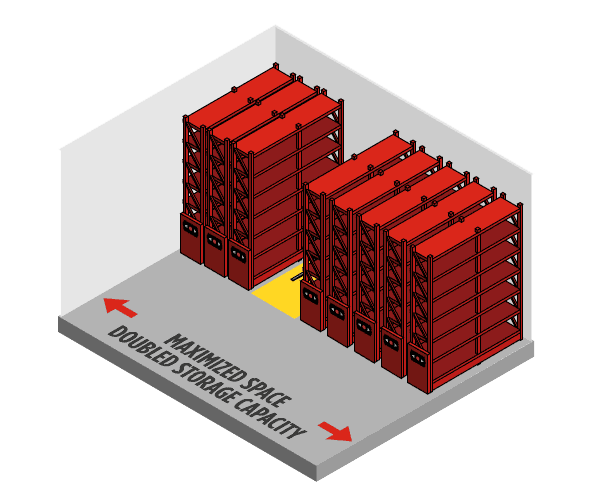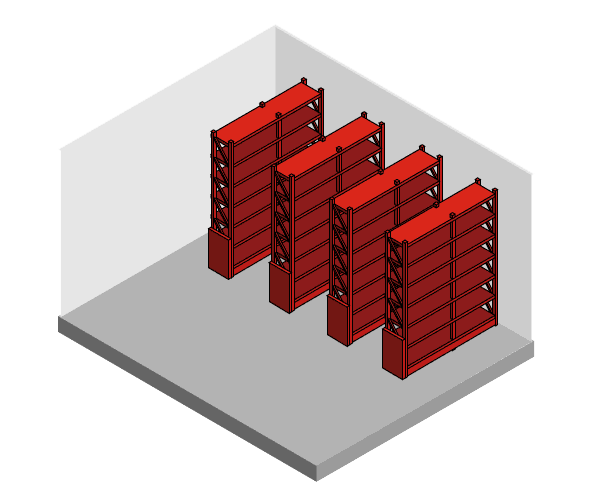
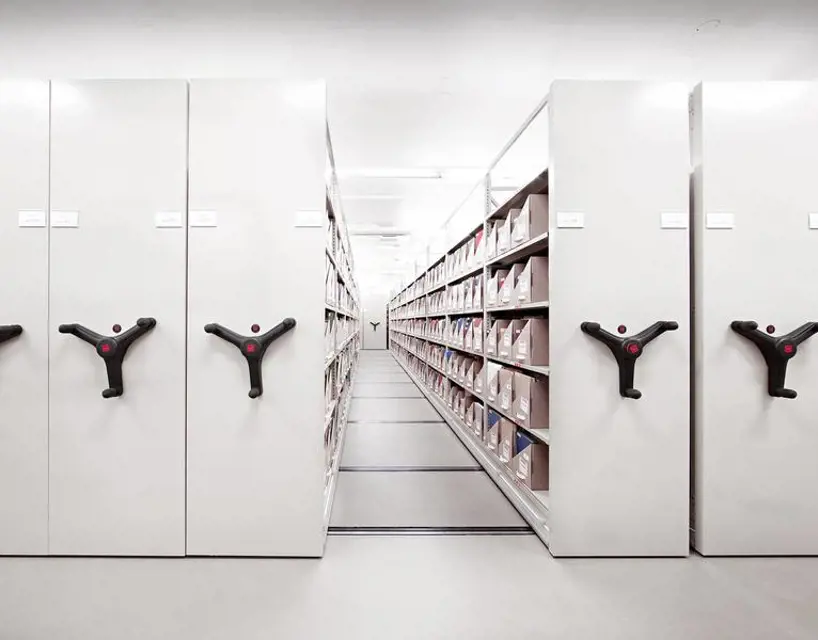
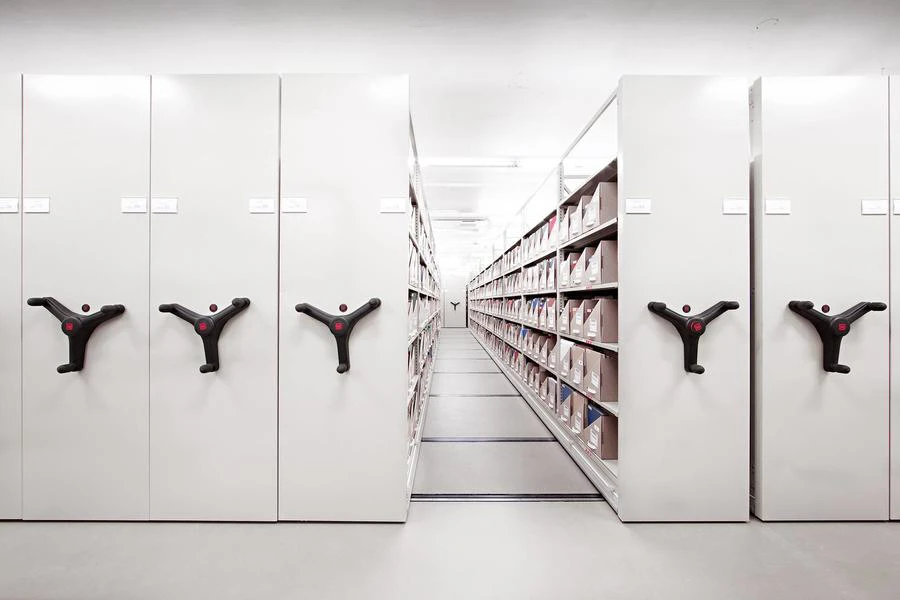
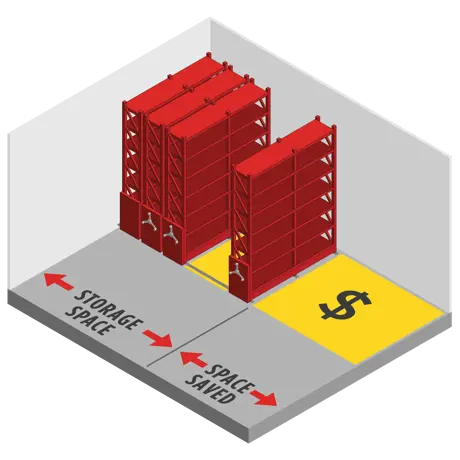
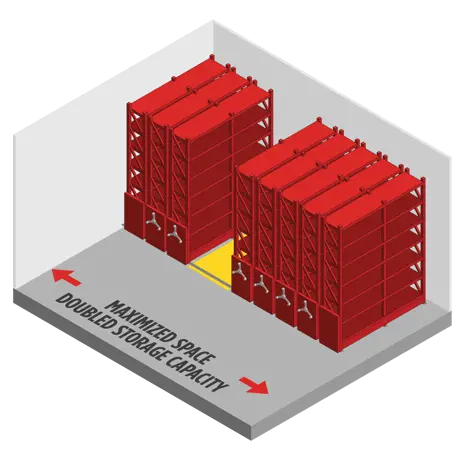
Traditional static shelving wastes up to 60% of hospital floor area solely on empty walkways between rows. Montel mobile carriages glide along flush tracks, consolidating multiple rows into a single movable aisle opened via crank or button.
Group fastest-moving pharmaceutical fast-movers close to packaging counters, reducing technician daily step counts by miles.
Easily move up to 30,000 lbs of heavy liquids and intravenous bulk goods with minimal finger pressure and ergonomic handle design.
Equipped with automatic obstruction sensors that immediately lock carriage motion if an object, foot, or supply cart enters the open pathway.
Hospitals are transitioning from scattered floor stockrooms to Centralized Service Centers (CSCs). High-density mobile pallet racks and high-bay shelving support bulk purchasing and just-in-time replenishment across health system networks.
The Drug Supply Chain Security Act (DSCSA) mandates full unit-level electronic tracking. Modern pharmacy shelving integrates RFID shelf antennas and pick-to-light LED modules, enabling instant location verification and lot-expiry alerts.
With high-value biopharmaceuticals and gene therapies surging, high-density shelving is increasingly engineered to operate directly inside refrigerated walk-in coolers and sub-zero storage chambers without mechanism freezing or rust.
Regulatory audits require immutable chain-of-custody logging. Advanced pharmacy storage integrates motorized tambours, biometric thumbprint scanners, and automated software locks that restrict narcotic vaults to authorized personnel.
Modern hospital engineering requires strict OSHPD (California) and IBC compliance. Montel anti-tip track anchoring, reinforced uprights, and safety shelf lips ensure critical medication vaults remain operational through major seismic events.
Pharmacy shelving no longer exists in a vacuum. It acts as the high-capacity staging backbone paired directly with robotic pill packagers, vertical carousel modules, and automated guided vehicles (AGVs) in cutting-edge healthcare networks.
Engineering parameters that hospital facilities directors, healthcare architects, and pharmacy operations executives must verify before signing off on storage retrofits.
Engineered structural anchoring accommodates severe seismic drift requirements, compliant with IBC specifications and the National Building Code of Canada.
Our surface-mounted modular rail decking evenly distributes live medication weights across elevated floors without needing invasive slab trenching or core drilling.
Layouts incorporate 36-inch minimum clear accessible corridors, automatic fire-suppression park modes, and 18-inch ceiling clearance from sprinkler heads.
Non-VOC powder coatings with antimicrobial properties resist bacteria growth. Fully documentation-compliant for healthcare LEED v4 sustainability credits.
Healthcare architects can drop comprehensive Montel Revit families directly into clinic design models, accelerating project signoffs.
Our certified teams follow strict containment and gowning procedures when executing installations inside occupied hospital facilities.
Building code regulations differ between states and provinces. Consult Montel Shelving Inc. engineering specialists and your local Authority Having Jurisdiction (AHJ) during early phase planning.
Detailed insights into floor capacities, sanitation guidelines, security protocols, and operational implementation for medical storage buyers.
Whether designing a newly constructed central inpatient pharmacy, retrofitting an outpatient clinic dispensary, or expanding an ISO cleanroom suite, our experienced engineers deliver turnkey layout solutions.