50%
Aisle Footprint Eliminated
Consolidates static access paths
100%
Pallet Capacity Increase
Within original building envelope
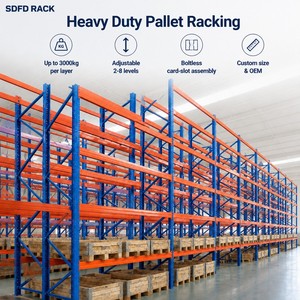
3,000kg
Payload Per Tier Support
Heavy-duty structural integrity
Q235B
High-Tensile Certified Steel
Seismic and fire compliant
Factory Direct Portfolio
Wholesale Powered & Heavy-Duty Storage Configurations
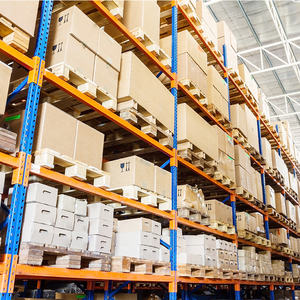
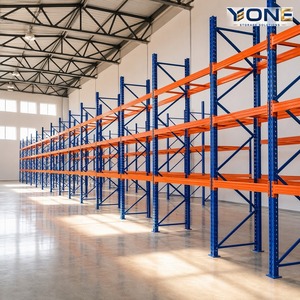
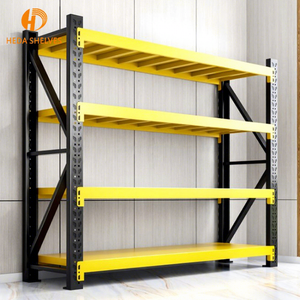
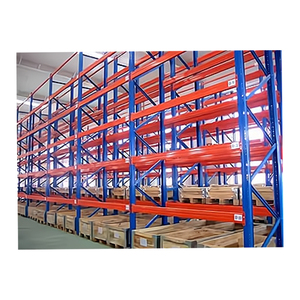
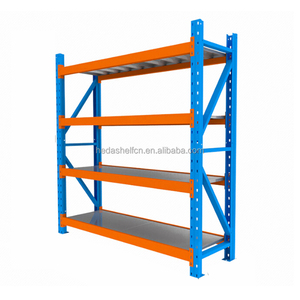
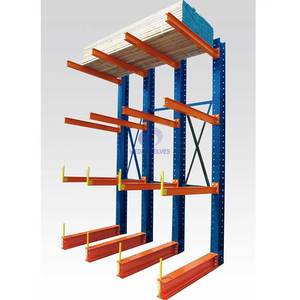
Precision-engineered industrial pallet racking, cantilever systems, and heavy-duty storage carriages engineered for turnkey integration in modern high-density distribution and manufacturing hubs.
Engineering Authority
The Kinematics of Powered Mobile Storage in Regional Wholesale
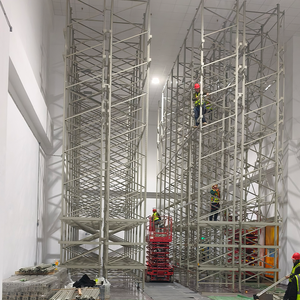
Wholesale distribution networks and industrial enterprises operating across Kingston and connected logistics corridors face acute real estate compression, escalating per-square-metre construction costs, and stringent thermal efficiency mandates. Powered mobile storage systems represent a fundamental departure from static industrial racking by mobilizing heavy-duty selective rack superstructures over in-floor structural guide rails. Driven by integrated electromechanical geared drive units, an entire bank of mobile carriages opens precisely when and where forklift or automated guided vehicle (AGV) access is required.
Conventional static storage layouts dedicate between 45% and 60% of total footprint exclusively to access aisles that remain idle during operational shifts. By collapsing these redundant access corridors into a singular dynamic, programmable aisle, powered mobile pallet racking increases usable storage volume by up to 100% within the exact same structural footprint. Alternatively, for facilities aiming to scale down physical plant overhead, the same volume of selective pallet inventory can be condensed into roughly half the floor space, directly cutting utility, HVAC, and commercial tax expenditures.
From an intralogistics engineering standpoint, each mobile carriage base is manufactured utilizing cold-formed Q235B high-tensile structural steel profiles. Carriage segments are coupled using CNC-machined flex-couplings to ensure equalized load distribution across high-grade steel rail tracks embedded flush within the structural concrete slab. Programmable Logic Controllers (PLCs) coordinate multi-axis motor synchronization, dynamic ramping, photoelectric safety light curtains, and tactile floor-level bumpers to achieve frictionless, fail-safe carriage transit under continuous full-load operating conditions.
System Engineering Parameters
- Carriage Load Rating Up to 30,000 kg / Carriage
- Structural Raw Material Q235B / Cold-Rolled Steel
- Traversing Velocity 4.0 - 5.5 m/min (Smooth Ramp)
- Floor Rail Tolerance ±1.0 mm per 10m run
- Drive Architecture Direct Axis Geared Motor + VFD
- Safety Sensor Envelope Dual Infrared + Proximity Bumpers
- Cold Chain Operating Range -30°C to +45°C Continuous
- Code Compliance IBC, CSA, NBC, CE Structural
Regional Application Blueprint
Localized Use-Cases Across Kingston's Commercial Hubs
Whether navigating maritime supply consolidation around the Kingston container terminal facilities or managing manufacturing stockpiles within industrial corridors, high-density powered mobile racking addresses specialized logistical demands.
Cold Storage & Food Logistics
Refrigeration electricity costs represent the largest variable expense in temperature-controlled warehousing. In cold storage distribution facilities throughout Kingston, compacting frozen food, perishables, and beverage kegs into powered mobile blocks cuts cubic volume thermal losses by up to 50%, maximizing pallet density per refrigerated kilowatt-hour.
Port Break-Bulk & Transshipment
Logistics depots supporting transshipment nodes manage rapid product turnovers coupled with sporadic dwell times. Selective high-bay racking mounted on mobile carriages offers immediate selective picking access to every single SKU without double-handling, providing containerized freight consolidators absolute inventory agility.
Pharmaceutical & Institutional Archives
Public sector facilities, academic institutions, and regional healthcare hubs require tamper-evident, dust-mitigated storage for patient records, narcotics, and controlled inventory. Powered carriages integrate PIN-code or RFID aisle locking, ensuring that access corridors only cycle for verified, credentialed personnel.
Industrial Manufacturing & MRO Parts
Heavy machinery assembly operations and automotive maintenance centers often struggle with odd-dimension dies, heavy raw materials, and high SKU fragmentations. Boltless multi-tier racks combined with heavy-duty mobile cantilever carriages allow rapid access to sheet metal, bar stocks, and specialized tooling.
Secured Armory & Tactical Depot
Government agencies and tactical facilities in the Kingston precinct leverage motorized carriage assemblies fitted with high-security biometric locks, anti-tip floor brackets, and seismic-rated structural steel framework for secure, organized weapon, gear, and evidence retention.
High-Density Museum & Fine Art Racks
Cultural preservation entities and heritage galleries mandate completely zero-vibration carriage movement to preserve fragile artifacts. Our specialized variable frequency drives (VFDs) deliver ultra-soft start and stop curves, guaranteeing zero impact on hung collections and delicate specimens.
Logistics Intelligence
Macro Trends Driving Powered Storage Across Regional Warehousing
Examining market forces, real estate capital costs, and automation milestones transforming industrial procurement priorities.
Urban Industrial Compression
Rising land lease valuations within core transportation corridors prevent horizontal warehouse sprawl. Engineering verticality and powered high-density mobile footprints delivers vital pallet expansion without acquiring additional acreage.
Integration with WMS & AGV Fleets
Modern powered mobile systems no longer rely solely on physical push buttons. Modern installations leverage industrial Ethernet and wireless I/O gateways to trigger aisle openings remotely via Warehouse Management Systems (WMS) and automated reach trucks.
Severe Energy Conservation Targets
Facility managers are held to rigorous carbon minimization standards. Compacting warehouses cuts lighting, air circulation, and temperature dissipation run-times, playing a measurable role in LEED certifications and corporate ESG scorecards.
Enhanced Workforce Ergonomics
Workplace safety standards mandate reduced repetitive stress and zero pinch hazards. Intelligent obstacle detection, optical safety sweep bars, and clear optical indication signals provide fail-safe physical buffers for pick-and-pack operators.
Procurement Guidance
Frequently Asked Questions: Powered Mobile Storage Systems
Technical considerations, installation parameters, and operational assessments for Kingston buyers, architects, and supply chain managers.
How much structural floor space can a powered mobile storage system realistically liberate? +
In typical selective pallet racking operations, up to 50% of the entire warehouse footprint is consumed by empty access aisles. By mounting racking superstructures on precision mobile carriages running along dedicated floor tracks, the facility only requires a single active dynamic aisle. This effectively doubles your pallet capacity within the existing square footage or compresses your storage footprint into half the space, freeing up prime operational zones for production, kitting, or staging without building expansion.
What floor and foundation specifications are required for powered mobile carriages? +
Because the concentrated load of mobile racking systems is transferred into floor rails rather than dispersed static footplates, slab structural integrity and levelness are critical. Existing slabs can be adapted using low-profile surface-mounted rails accompanied by ramped decking that requires zero slab trenching. For ground-up new builds, recessed guide tracks are embedded directly flush with the finished concrete pour, designed to meet rigorous FF/FL (floor flatness and floor levelness) tolerances compliant with international building codes.
What active safety systems protect warehouse personnel inside the moving aisles? +
Safety redundancy is built into every carriage bank. Standard safety features include full-height photoelectric light curtains positioned along the carriage faces that halt carriage travel instantly if a beam is broken. Additionally, floor-level infrared photo sweeps, physical emergency stop kick-plates, and torque-monitoring current sensors detect foreign obstacles or dropped cartons on the track, immediately locking carriage motors and transmitting an alert to the master control panel.
What differentiates manual, mechanical-assist, and powered electric mobile systems? +
Manual systems feature basic handles suitable for small office filing or light-duty parts rooms under 1,000 kg. Mechanical-assist uses a gear-reduction crank handle (such as 3-spoke SafeCrank assemblies) allowing a single person to move up to 5,000–10,000 kg with modest manual effort. Powered mobile storage systems utilize electric gear motors managed by variable speed drives and microprocessors. They are essential for industrial high-bay racks, pallet operations exceeding 10 tons per carriage, cold storage facilities, and high-frequency automated logistics hubs.
Can powered mobile racking function reliably in blast freezers and cold storage? +
Yes. Our cold chain mobile racking packages are specifically engineered to perform seamlessly in sub-zero environments down to -30°C (-22°F). These variants utilize specialized low-temperature lubricants, thermal internal heaters within PLC enclosures, sealed IP65 drive motors, and low-temperature ductile structural steel alloys to eliminate embrittlement and maintain smooth, condensation-free operation.
Are structural systems compliant with seismic and building fire safety regulations? +
All structural designs are developed in strict adherence to international building standards (IBC, CSA, and National Building Codes). Systems include anti-tip base anchors, top-tie structural guides for tall aspect-ratio frames, and automated night-parking settings that evenly park carriages across the floor to ensure proper fire sprinkler water penetration patterns during non-operational hours.
Why Partner With Us
Our Engineering Heritage & Manufacturing Edge
Decades of intralogistics manufacturing excellence, turnkey CAD engineering, and uncompromised structural reliability.
Custom Structural Sizing
No two warehouse topologies are identical. Our engineering team designs custom upright heights, carriage clear widths, and beam tier configurations tailored to match your specific pallet dimensions, forklift reach limits, and ceiling trusses.
Free 2D/3D BIM & Capacity Audits
Before purchasing or committing capital, we generate complete 2D elevation diagrams, 3D clearance simulations, and Revit/BIM models to help architects, project engineers, and facility teams accurately calculate ROI and pallet gain.
Factory-Direct Turnkey Supply Chain
As direct manufacturers, we maintain comprehensive control over metallurgical testing, automated powder coating, electrical programming, and logistics packaging, delivering dependable lead times and containerized wholesale pricing directly to Kingston buyers.