Featured Industrial Pallet Racking & Material Handling Systems
Engineered to international safety standards (RMI, FEM 10.2.02, AS4084), our custom cold-rolled high-tensile steel racking frames provide maximum cubic footprint optimization, ultra-heavy load endurance, and integrated warehouse automation capability.
Strategic Engineering Architecture: The Core of High-Yield Pallet Storage
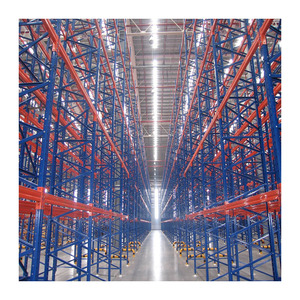
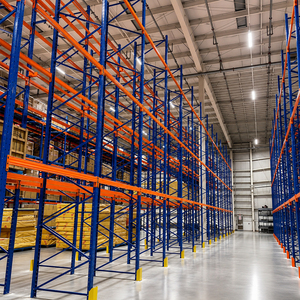
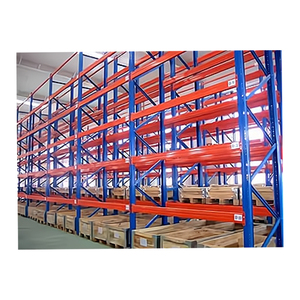
Modern distribution centers, 3PL facilities, and global FMCG manufacturing hubs require storage solutions that surpass standard catalogue configurations. As a high-capacity custom OEM pallet rack exporter and wholesaler, our structural design principles reflect over three decades of mechanical innovation. Standard selective racking systems often allocate up to 60% of real warehouse floor area to wide forklift transport lanes. By integrating high-precision cold-rolled profile uprights, engineered seismic footplates, and micro-adjustable interlocking box beams, we convert wasted vertical air-rights into heavy-duty storage capacity.
Our upright columns are fabricated exclusively from certified high-tensile Q235B and Q355B structural steel alloys. Through precision multi-stage roll-forming tooling, cold-work hardening generates exceptional cross-sectional stiffness with optimized metal gauge thickness. This metallurgical superiority prevents frame deflection under dynamic forklift impacts, structural harmonic loading, and cyclic fatigue, delivering unmatched longevity across high-throughput supply chains.
Finite Element Analysis (FEA)
Every frame configuration is simulated under multi-axial load scenarios, assessing non-linear buckling, seismic base shear stress, and deflection criteria aligned with ANSI/RMI MH16.1 specifications.
Thermoset Powder Coating
Electrostatic automated powder-coating lines apply 60-80 micron thickness cross-linked polyester coatings, resisting chemical corrosion, severe humidity, micro-cracking, and mechanical abrasion.
Robotic Laser Punching
Featuring teardrop or diamond 50mm/75mm adjustable pitch indexing with 0.1mm punch tolerance, facilitating rapid beam reconfiguration while maintaining positive structural lock safety.
Future Procurement Trends in Industrial Storage Systems (2025–2030)
B2B procurement departments and warehouse developers face shifting operational parameters: escalating cost per square meter, labor availability constraints, and tighter green logistics mandates. Future procurement strategies prioritize the following dynamics:
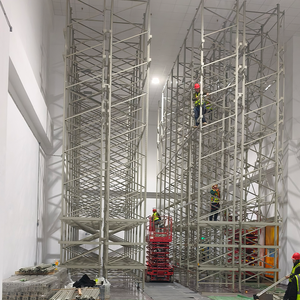
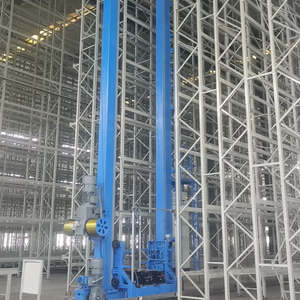
1. Transition from Static Aisles to Dense Powered Mobile & High-Bay AS/RS: Buyers are phasing out standard wide-aisle configurations in favor of high-density mobile racking, radio shuttle drive-in bays, and crane-serviced high-bay structures. By compressing dynamic carriages on embedded ground rails, operations eliminate static access corridors, reclaiming up to 50% of real estate footprint or doubling capacity without facility expansion.
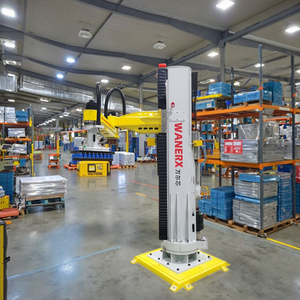
2. Hybridization of Robotic Palletization and Modular Racking: As showcased by our integrated 70kg automated robotic column-stacking systems, end-of-line packaging and raw rack storage are merging. Procurement heads increasingly contract single-source OEM suppliers capable of harmonizing mechanical pallet rack tolerances with autonomous guided vehicles (AGVs) and robotic palletizers.
3. Life Cycle Decarbonization and Recyclability (ESG Compliance): Driven by international building benchmarks like LEED v4 and strict Scope 3 industrial supply chain audits, racking procurement mandates sustainably processed scrap steel, non-toxic heavy metal-free powder coatings, and zero-loss cold rolling efficiency.
| Storage Racking Architecture | Space Utilization | Selectivity Ratio | Handling Equipment Compatibility | Ideal Application Profile |
|---|---|---|---|---|
| Standard Selective Pallet Racking | 40% – 45% | 100% (Instant Direct Access) | Standard Counterbalance, Reach Trucks | High SKU variety, fast-paced retail & FMCG distribution |
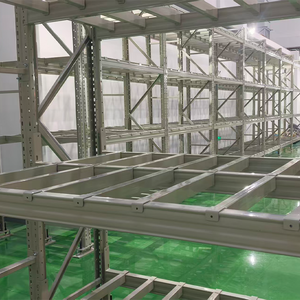
| Heavy-Duty Mobile Pallet Racking | 80% – 85% | 100% (Dynamic Moving Aisle) | Reach Trucks, Articulated Forklifts | Cold storage, pharmaceuticals, expensive real estate footprints |
| Drive-In / Drive-Through Systems | 65% – 75% | Low (FILO / FIFO batch logic) | Specialized Narrow Counterbalance | Homogeneous bulk inventory, seasonal goods, food processing |
| Automated Radio Shuttle Racking | 85% – 90% | High Batch Efficiency (Automated FIFO/FILO) | Internal Autonomous Shuttle Cart + AGV | High-throughput distribution hubs, beverage, raw chemical production |
Engineering Capabilities & OEM Enterprise Competencies
As a global OEM exporter and wholesale distributor, our manufacturing facility merges comprehensive fabrication scale with engineering consultation:
Rapid 24h CAD & BIM Engineering
Our dedicated engineering department generates customized 2D spatial layouts, structural calculations, and 3D Revit models within 24 hours of receiving site blueprints, preventing clearance conflicts.
Full-Cycle Export & Logistics
Exporting to over 60 countries across North America, Europe, Australia, and Southeast Asia. We supply ocean-safe steel banding, plastic film packaging, and container stowage plans.
Certified Field-Proven Quality
Fully compliant with ISO9001, CE, and AS4084 criteria. Every steel batch undergoes destructive coupon testing, yield-strength validation, and weld penetration testing.
Frequently Asked Questions (FAQ)
Key technical, engineering, and logistic questions reviewed by procurement professionals before placing custom OEM pallet racking orders.
How do you verify weight loading limits and safety factors?
Our load tables adhere strictly to ANSI/RMI MH16.1 and FEM standards. Structural calculations integrate dead load, live pallet loads, seismic horizontal loads, and wind shear (for rack-supported buildings), applying standard safety factors between 1.5 and 1.95.
Can you manufacture custom dimensions and color schemes?
Yes. As an OEM manufacturer, upright column depth (600mm to 1500mm+), frame height (up to 16,000mm single section), steel thickness (1.5mm to 3.5mm), and custom RAL electrostatic powder colors can be calibrated to your exact operational specifications.
What documentation accompanies international export shipments?
Every commercial wholesale export includes comprehensive Mill Test Certificates (MTC), coating thickness verification reports, assembly and anchor bolt layout drawings, bill of materials (BOM), and certified structural warranty sheets.
How are existing concrete slab conditions evaluated?
We review your concrete slab thickness, compressive strength (PSI/MPa), flatness tolerances (DIN 18202 or ASTM E1155), and sub-base stability to size base plates and expansion anchor patterns correctly, preventing floor punching and shear failures.