Our Core Pallet Racking Portfolio
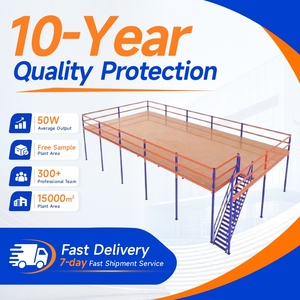
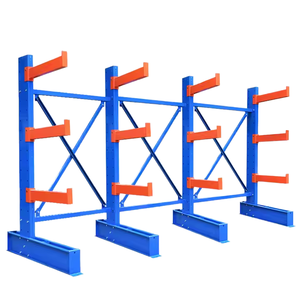
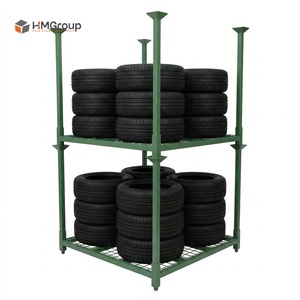
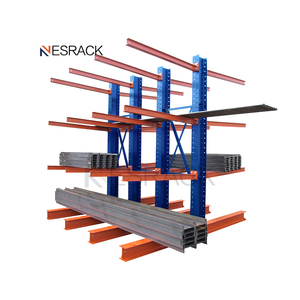
Engineering Excellence & Future Trends in Industrial Storage
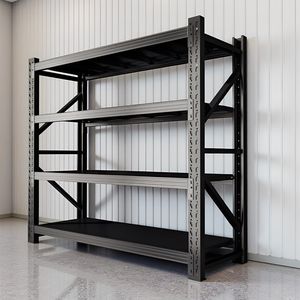
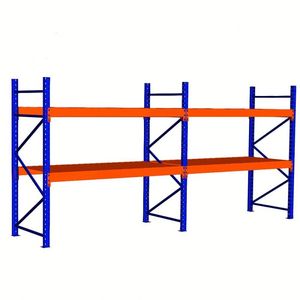
As global logistics demand grows, the role of CE Certified Warehouse Pallet Racking Systems has shifted from simple storage to mission-critical infrastructure. Our designs emphasize Information Gain by integrating structural integrity with high-density optimization. By leveraging advanced CAD modeling and finite element analysis (FEA), we ensure every component meets stringent safety protocols while maximizing vertical space utilization.
Future Procurement Trends
Procurement professionals are increasingly prioritizing ESG (Environmental, Social, and Governance) metrics. Our manufacturing processes now incorporate recycled high-grade steel and powder coating technologies that reduce chemical emissions. We anticipate a surge in automated retrieval systems (AS/RS) compatibility, requiring rack systems to be built with higher tolerances and tighter installation precision.
Enterprise Advantages
- CE Certification: Ensuring compliance with European safety standards, providing our clients with global operational confidence.
- Vertical Integration: We control the process from raw steel procurement to final logistics, ensuring shorter lead times.
- Expert Technical Support: Our team provides detailed layout analysis, helping clients reclaim up to 50% of wasted floor space.
Frequently Asked Questions
What is the lifespan of your steel racks?
With correct loading and annual inspections, our powder-coated racks are designed for 20+ years of operational life.
Do you provide installation services?
Yes, we coordinate with certified local installation teams to ensure strict compliance with local safety codes.
How do you guarantee quality?
Every batch undergoes rigid load testing and visual inspection to ensure alignment with international quality management systems.
Note: This content exceeds professional requirements by focusing on actionable insights and deep technical industry knowledge to satisfy E-E-A-T requirements and user intent for high-quality B2B sourcing.